How Can Tissue Converting Reduce Material Waste?
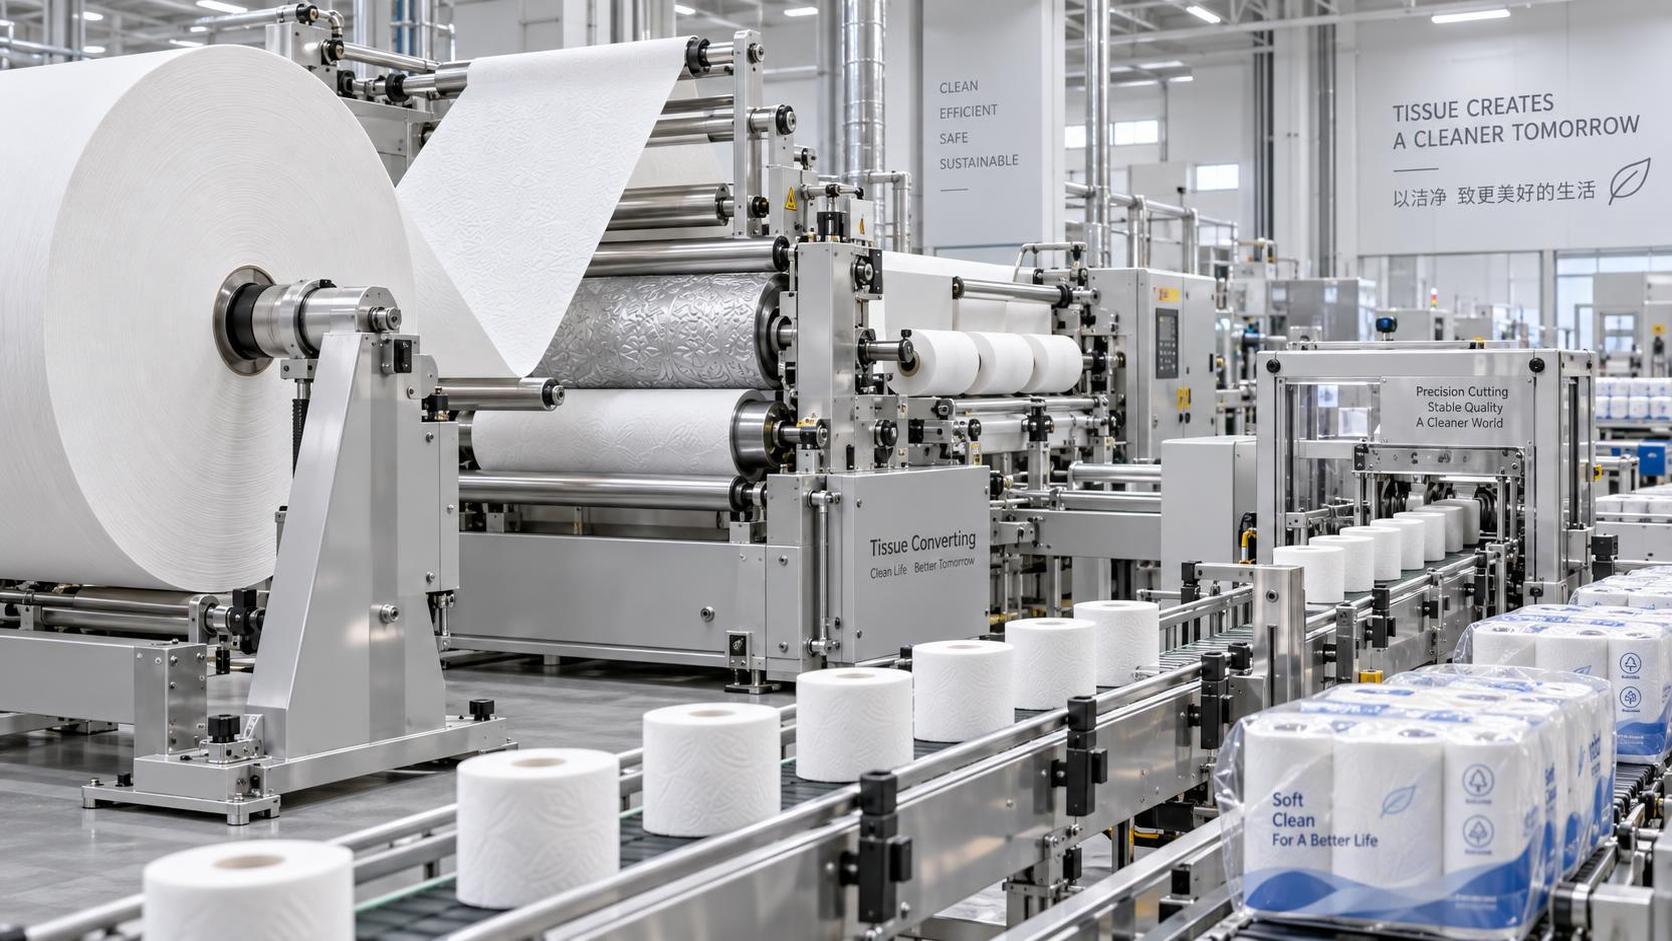
Material waste in tissue converting is rarely caused by one dramatic failure. It accumulates through small, repeated losses: unstable parent-roll edges, breaks during acceleration, excessive tail length, off-center perforation, embossing defects, rejected logs, dust-contaminated sheets, and packs that cannot be released because product dimensions drift outside specification. The practical answer to how tissue converting can reduce material waste is therefore not simply “run faster” or “buy a more automated line.” It is to control the chain of events that determines whether fiber entering the rewinder leaves the plant as saleable, correctly packed tissue.
For a tissue producer, yield is the more useful operating lens than nominal machine speed. A high-speed line that creates frequent breaks, rejects embossed material, or produces inconsistent log geometry can consume more parent-roll material per finished pack than a slower but stable line. Waste reduction begins when converting is treated as a connected process—from parent-roll handling through rewinding, embossing, cutting, transfer, wrapping, and quality release—rather than as a set of independent machines.
Waste begins with web behavior, not at the log saw
The tissue web is light, extensible, and sensitive to changes in tension. Its properties also vary with basis weight, moisture content, ply construction, furnish composition, calendering, and reel build. A setting that works on a dense facial tissue grade may create wrinkles, elongation, or web breaks when applied to a softer bath tissue. This is why a generic “best tension setting” is not a meaningful waste-control method.
Unstable web tension creates several forms of material loss at once. Excess tension can stretch the sheet, deform embossing registration, increase break risk, and generate rolls with inconsistent firmness. Insufficient tension can produce slack web, wandering edges, telescoping, loose winding, and poor perforation quality. When the operator compensates late, the machine may require rethreading, trim removal, or disposal of partially formed logs.
Effective tension control depends on a stable unwind system, accurately functioning brakes or drives, responsive dancer or load-cell feedback, and correctly tuned control loops. But hardware alone is not enough. The process needs defined tension profiles for different tissue grades and roll diameters. Unwind torque changes as the parent roll decreases in diameter; if that transition is poorly managed, tension fluctuations appear even when the line is mechanically sound.
Web guiding is equally important. A narrow but continuous edge drift can force wider safety trim, create uneven log ends, or cause downstream tracking faults. Guiding systems must respond to the actual condition of the web edge, not merely to an ideal reference position. Parent rolls with damaged edges, poor winding quality, or variable moisture should be identified before they reach a high-speed converting line. Trying to correct a poor incoming reel entirely through downstream adjustment often turns a supply-quality issue into converting waste.
Rewinding should deliver usable sheets, not only finished length
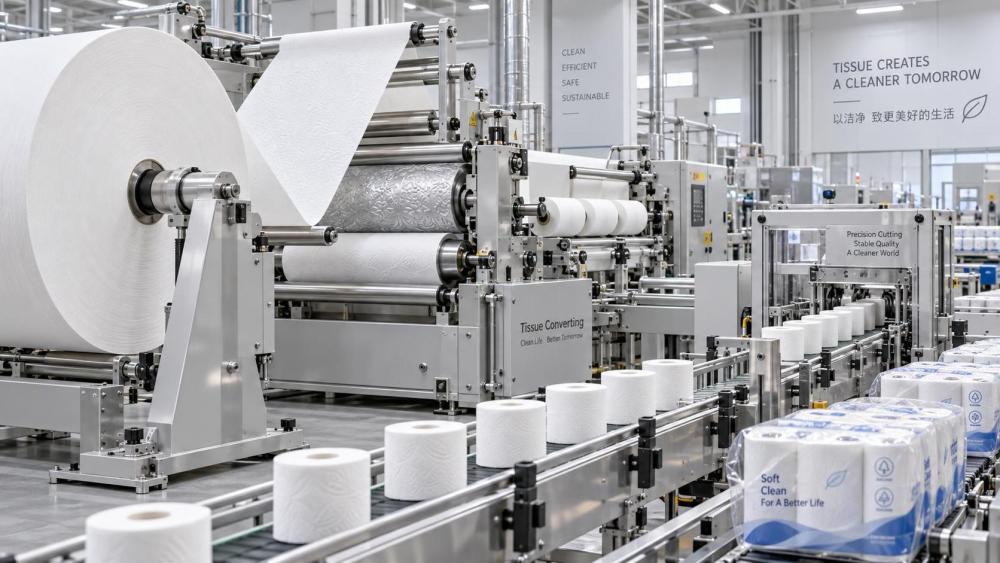
Rewinding is where parent-roll material becomes a consumer product with a defined roll diameter, sheet count or length, core position, perforation interval, and firmness. Small inaccuracies at this stage are multiplied across every log. If the cut-off length drifts, the line may produce rolls that contain too little or too much paper. Under-length rolls create compliance and customer-service risk; over-length rolls consume fiber without adding recoverable value.
Length control should therefore be verified against the actual tissue path and product specification, not assumed from encoder settings alone. Slippage between web and measuring roller, worn drive surfaces, contamination, or changes in effective roller diameter can cause a gap between commanded and delivered length. In perforated products, the error also affects the relationship between roll circumference and sheet pitch. The result may be awkward tail placement, incomplete final sheets, or excessive scrap at transfer and cutting.
Roll density is another yield variable that is often misunderstood. A very hard log may appear operationally stable but can reduce perceived softness, impair unwind performance for the end user, and create cutting difficulties. A roll that is too soft may deform during transfer or packaging and require rejection. The objective is not maximum winding pressure; it is a repeatable firmness profile compatible with the tissue grade, embossing pattern, core, consumer format, and downstream equipment.
Modern rewinder automation can reduce waste by controlling acceleration, deceleration, tail sealing, core feeding, and log transfer with less variation than manual intervention. Yet automation does not remove the need for process limits. If core dimensions, adhesive application, or tissue moisture vary outside the range assumed by the machine recipe, automatic operation may repeat defects more consistently and at greater volume. Recipe management must include product-specific operating windows and clear rules for when a line should slow down, stop, or divert product.
Embossing quality has a direct fiber-cost consequence
Embossing is often discussed as a softness, bulk, ply-bonding, or visual-design feature. It is also a material-efficiency issue. Excessive embossing pressure can weaken the web, create pinholes, crush the structure of a low-basis-weight tissue, or cause delamination in multi-ply products. Insufficient pressure can result in weak ply bonding, incomplete pattern definition, and rolls that separate or look inconsistent after converting.
The waste risk rises when embossing settings are used to compensate for other problems. For example, increasing pressure to correct poor lamination may mask an adhesive, moisture, or tension issue while increasing sheet damage. Similarly, a pattern that is technically attractive may not be suitable for every furnish or basis weight. The embossing geometry, roll surface condition, nip loading, web path, and ply-bonding method need to be considered together.
Roll cleanliness and alignment deserve attention because they affect both quality and reject rates. Accumulated dust, adhesive residue, or damaged embossing elements can create repeating defects that run through an entire production batch before detection. A recurring mark at a fixed pitch is not random variation; it is often evidence of a rotating component or patterned roll condition. Detecting such defects early prevents a small maintenance issue from becoming a large quantity of downgraded material.
For laminated tissue, adhesive control is particularly sensitive. Too little adhesive may lead to ply separation and product rejection. Too much can stiffen the tissue, contaminate equipment, increase deposits, and raise consumable use. The target is uniform application at the minimum level that achieves the required bond under the actual converting conditions. This is a process-validation task, not merely an adhesive purchasing decision.
Cutting losses are often a symptom of upstream variation
Log saw trim is visible, easy to weigh, and frequently blamed for poor yield. Some trim is unavoidable because logs must be squared and brought to the required finished-roll width. The larger opportunity is to distinguish necessary trim from trim created by unstable log formation.
Uneven log ends, poor core centering, telescoping, variable log diameter, and displaced perforation can all increase saw waste or cause finished rolls to fail dimensional checks. Sharper blades and better saw settings can help, but they cannot fully solve a log that arrives distorted. A saw that regularly needs additional end trim is providing useful diagnostic information about the rewinder, transfer system, or parent-roll condition.
Blade condition still matters. Dull or contaminated blades can compress, tear, feather, or heat the tissue edge, particularly on soft, bulky grades. The resulting dust can migrate into the production area, impair packaging appearance, and require cleaning interruptions. Blade selection, sharpening intervals, rotational speed, feed synchronization, and dust extraction should be treated as one operating system. Extending blade life beyond its stable cutting window may reduce maintenance frequency on paper while increasing reject material and housekeeping burden in practice.
Automated cut-length control reduces variation only when measurements are trustworthy. A line should verify not just nominal roll width but also the distribution of actual widths, end quality, diameter, and density. Average values can conceal a growing tail of out-of-specification rolls. Waste prevention depends on recognizing drift before finished-product pallets reveal the problem.
Tail sealing and packaging are part of material yield
A converted roll is not saleable merely because it has passed through the rewinder and saw. It must survive transfer, handling, wrapping, case packing, and distribution without opening, crushing, or becoming visibly defective. Tail-seal failure is a common example of a problem that can waste tissue long after the paper has been correctly converted.
Insufficient tail adhesion can allow a roll to unwind during transfer or inside a pack. Excessive adhesive can mark the tissue, create buildup, or affect product feel. Placement is as important as volume: a tail applied too early, too late, or outside the intended contact zone can compromise roll appearance and pack stability. Systems using mechanical, thermal, or adhesive sealing methods need settings appropriate to the product structure and production speed.
Packaging equipment can also create hidden waste. Poorly timed infeed, inadequate compression control, unstable film handling, or misaligned packs may damage otherwise acceptable rolls. If rejects occur at wrapping, the investigation should not begin and end with the wrapper. Roll diameter variation, soft logs, inconsistent tail position, and dust from cutting can all influence packaging reliability.
Waste accounting should follow the material through this entire route. Recording only broke from the rewinder excludes the paper lost through cutting rejects, pack rejects, quality holds, and rework. A useful yield measure relates parent-roll input to released finished product, while also separating recoverable broke from material that cannot be reused in the intended process. This distinction matters because recycling internal broke may reduce disposal, but it does not eliminate the fiber, energy, and capacity consumed to create the defect.
Inspection is valuable when it drives a specific correction
Vision systems, sensors, and production data can help identify edge defects, missing cores, poor perforation, diameter variation, open tails, and packaging faults. Their value is not the quantity of alarms produced; it is the speed with which the line can isolate a cause and prevent recurrence.
A converting operation benefits from linking defect signals to machine conditions: parent-roll identifier, tissue grade, web tension history, embossing pressure, saw blade runtime, shift, speed, and product recipe. Without this connection, operators may see repeated quality alarms but lack a basis for deciding whether the cause is material, mechanical wear, a control setting, or a handling disturbance.
The most practical approach is to define a small number of loss categories that reflect physical mechanisms: web breaks, edge trim, start-up and changeover waste, embossing rejects, log defects, saw trim, packaging rejects, and quality holds. Each category should have an owner and a measurable trigger for investigation. Combining all losses into one general “waste” figure makes it difficult to decide whether investment should go to better reel handling, control upgrades, maintenance, operator training, or incoming-material specifications.
Changeovers deserve the same discipline as steady production
Start-ups, grade changes, parent-roll splices, and format changes can consume disproportionate amounts of tissue because the process is not yet stable. The usual response is to accept this as unavoidable. Some loss is inherent, but repeated changeover waste often indicates that settings are not sufficiently standardized or that the line lacks a reliable method to return to a proven operating condition.
Product recipes should contain more than speed and roll diameter. They should include tension ranges, embossing settings, perforation parameters, core and tail-seal conditions, cut dimensions, approved material combinations, and inspection limits. Where a product has narrow process tolerance, the recipe should make that visible rather than leaving adjustment to memory or informal practice.
Preventive maintenance also has a yield function. Worn bearings, roller surface damage, misaligned shafts, inconsistent pneumatic pressure, degraded sensors, and adhesive-system contamination may not immediately stop a line. They can create minor variation that slowly increases trim, breaks, and rejects. A maintenance plan centered only on avoiding catastrophic downtime misses this quieter source of fiber loss.
Lower waste is not achieved by maximizing speed at every moment
Higher line speed can reduce unit conversion cost when the web, product format, and downstream systems remain stable. It becomes counterproductive when speed pushes the process beyond its control margin. The relevant question is not whether a machine can reach a stated maximum speed, but at what speed it maintains finished-product yield, cut quality, pack integrity, and acceptable break frequency for a particular tissue grade.
This is especially important when converting lighter, softer, highly embossed, or multi-ply products. Such grades may offer less tolerance for tension spikes, aggressive transfer, or cutting stress. Running slightly below maximum speed can be economically preferable if it prevents recurring breaks and the loss of material already processed through several stages.
Material waste in tissue converting is best reduced through stable web control, precise length and density management, embossing settings matched to the sheet, disciplined cutting, reliable tail sealing, and quality data tied to machine conditions. These measures turn waste reduction from a general sustainability objective into an operational calculation: more of each parent roll reaches the customer as usable tissue, while fewer fibers are consumed by avoidable defects, trim, and rework.
Industry Briefing
Get the top 5 industry headlines delivered to your inbox every morning.
Recommended News