Can print intelligence reduce waste in corrugated packaging?
Yes. Print intelligence can reduce waste in corrugated packaging when it helps operators detect defects earlier, shorten setup, and prevent unsuitable sheets from moving into finishing. Its value is greatest when production data leads to a timely decision: adjust the press, isolate a suspect batch, correct an artwork file, or stop a repeat defect before more board is consumed.
The size of the opportunity depends on where waste occurs. A plant losing material to color variation, print registration, or unidentified print defects may benefit directly from better inspection and process data. A plant whose largest losses come from warped board or poor creasing may need to connect print information with corrugating and converting records before it can address the cause. In either case, a dashboard alone does not reduce scrap; the production team needs reliable measurements and a practical way to act on them.
Where production data can prevent waste
Corrugated packaging presents a difficult printing surface. Liner characteristics, flute structure, moisture, board flatness, and surface condition can affect how a sheet feeds and how ink appears. A print system may perform consistently while incoming material changes enough to alter the result. Equally, a stable board grade can produce inconsistent output if print settings, maintenance, or artwork handling vary between shifts.
Industrial print intelligence for corrugated operations brings these observations together at a level that operators and engineers can use. Depending on the equipment, that may include job data, press settings, inspection images, production counts, alarms, and information about the board being printed. The useful question is whether those records help explain a defect and narrow the response.
Reducing setup and approval losses
Setup waste accumulates when a press needs repeated adjustments before the output meets the approved specification. For repeat work, a searchable record of the previous job can provide a better starting point: board grade, artwork version, color settings, machine configuration, and any adjustments made during the run.
Those settings should be treated as a starting point, not an automatic guarantee. A different liner, ink condition, or board profile can change the result. The benefit comes from making prior production knowledge available to the operator and showing which conditions have changed. If a system retrieves a previous recipe without identifying those differences, it can reproduce the wrong settings just as quickly as the right ones.
For jobs requiring color approval, measurement data can also make acceptance more consistent than visual judgment alone. The evaluation team should establish which color references, measurement locations, and tolerances are meaningful for the customer and substrate. Corrugated surfaces are variable, so a measurement method must account for that variability before an alert can be used as a basis for rejecting sheets.
Catching defects before they travel downstream
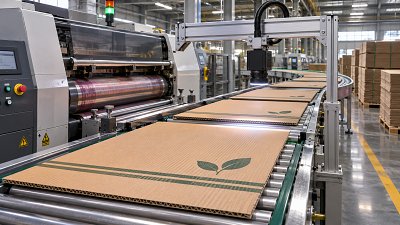
Inspection can identify missing print, streaks, registration problems, incorrect artwork, or other visible defects while a job is running. Its waste-reduction effect depends on the time between the first defective sheet and intervention. An alert that arrives after a large batch has already passed through the press has limited preventive value, even if the defect is recorded accurately.
Location matters as well as speed. If defective sheets can be identified and segregated before die-cutting or folder-gluing, the plant may avoid spending additional time and materials on boxes that cannot be shipped. Inspection after finishing can still protect the customer, but it offers fewer opportunities to avoid downstream conversion losses.
Automated inspection also needs a clear response procedure. Teams should know which defects require an immediate stop, which allow continued production within an agreed tolerance, and who decides when an alert is ambiguous. Excessive false alarms can interrupt production and encourage operators to disregard the system; missed defects can leave the plant with a false sense of control.
Connecting print defects with board and finishing conditions
A print defect is not always caused by the press. Poor board flatness can affect feeding and print consistency. Damage or variation in the liner may change the printed appearance. A registration problem observed at die-cutting may involve print placement, sheet movement, cutting setup, or a combination of factors.
Linking the print job to a board batch and to relevant finishing results helps engineers investigate those possibilities. For example, if a defect appears across several print jobs using the same board batch, material condition becomes a useful line of inquiry. If it follows a particular machine setting across different batches, the press setup deserves attention. Neither pattern proves the cause on its own, but it gives the team a more focused place to investigate.
Traceability does not require every machine to share a single control system. It does require identifiers that survive handoffs: a job number, artwork version, board batch or roll reference where available, production time, and a way to associate suspect sheets or pallets with finishing results. If records cannot be matched reliably, a sophisticated analysis may still leave engineers guessing which material was affected.
When intelligence is likely to pay for itself
The strongest candidates are operations with recurring, measurable losses and enough variation for better decisions to matter. Frequent job changes can make setup records valuable. High print coverage or demanding graphics can make early defect detection more consequential. Jobs that pass through multiple converting steps benefit from identifying suspect material before additional work is performed.
Short and customized runs present a particular opportunity, but they do not automatically justify a new press. Digital printing can remove plate-making from suitable jobs and support version changes, potentially reducing obsolete inventory or overproduction when order quantities are uncertain. The total result still depends on setup practices, ink consumption, production speed, board compatibility, and finishing requirements. An operation can also improve waste performance on an existing press by capturing better setup and inspection data.
Conversely, the value of print intelligence may be limited when print-related losses are already small, jobs are highly stable, or the dominant source of scrap lies elsewhere. A camera that detects a defect cannot correct a damaged print component or unsuitable board. It may reveal the problem sooner, but maintenance, material control, or a process change is still needed to remove the cause.
Some interventions can shift waste rather than eliminate it. Tighter inspection limits may reduce customer complaints while increasing the number of sheets rejected internally. More frequent cleaning may improve print quality while consuming time and materials. The engineering decision should consider whether the added rejection or maintenance prevents a larger loss, including rework and downstream processing.
How to evaluate a system against a real waste problem
Start with a defined loss category and a production decision that could change it. “Reduce waste” is too broad for a useful equipment trial. “Identify recurring streaks early enough to isolate affected sheets before die-cutting” provides a clearer basis for assessing inspection coverage, alert speed, and traceability.
A technical evaluation should follow a small set of representative jobs through the process. Include the board grades, graphics, run lengths, and operating conditions that make the problem difficult. If a proposed system relies on images, assess performance on the actual surfaces and print coverage involved; a clean demonstration sample may not represent the variability of production board.
Ask suppliers and internal teams to show how the following questions will be answered in the intended workflow:
- What can be detected or measured? Identify the defect types, inspection area, resolution needs, and known limitations. Check how the system handles acceptable variation in the substrate.
- How quickly can someone act? Establish where an alert appears, how the affected material is located, and whether the line can stop or segregate sheets in time.
- Can records be connected? Check how job, artwork, board, press, and finishing identifiers are captured, including manual steps and missing data.
- Who maintains the rules? Determine how tolerances, reference images, job recipes, and user permissions are set and updated when specifications change.
- Can the output be investigated? Confirm that engineers can review the underlying events and export usable records, rather than relying solely on a summary score.
Integration deserves particular attention when equipment comes from different suppliers or includes older machines. A system may receive production counts but not the settings needed to explain a defect. Manual entry can fill some gaps, although it adds workload and depends on consistent use. Evaluate the information available on the actual line, including how clocks, job changes, and material handoffs are recorded.
Measure the result without confusing detection with prevention
Before changing the process, establish a baseline for the chosen jobs and define what counts as waste. Track setup sheets, rejected production sheets, rework, and material discarded after finishing separately where possible. A single scrap total can hide a useful improvement at the press or obscure a new loss introduced downstream.
Compare results over a representative period and account for changes in job mix. A period with more complex graphics or shorter runs may produce a different waste rate even if the equipment performs the same way. Useful measures can include rejected sheets per job or as a share of sheets produced, setup sheets per changeover, time from defect onset to intervention, and the quantity of suspect material reaching finishing. Use the measures that fit the problem, with consistent definitions before and after the change.
Costs should be assessed across the same boundary. A reduction in discarded board is valuable, but the investment case may also depend on avoided reprints, less converting of defective sheets, inspection labor, maintenance, software support, and any additional consumables. Keep customer returns or avoided overproduction separate unless there is enough evidence to connect them to the change.
The best next step is often a controlled trial on a recurring loss, with operators, quality staff, and finishing personnel agreeing in advance on the response to an alert. If the system can detect the problem, identify affected material, and support an intervention that reduces total loss under normal production conditions, the case for wider deployment becomes much stronger.
Industry Briefing
Get the top 5 industry headlines delivered to your inbox every morning.
Got questions about the latest insights discussed here, or seeking customized strategic advice for your business? Drop us a line below, and let the think-tank experts at IPPS help you out.
“We respect your privacy. Your information is strictly confidential.”
Recommended News