How paperboard grade affects carton converting machinery selection
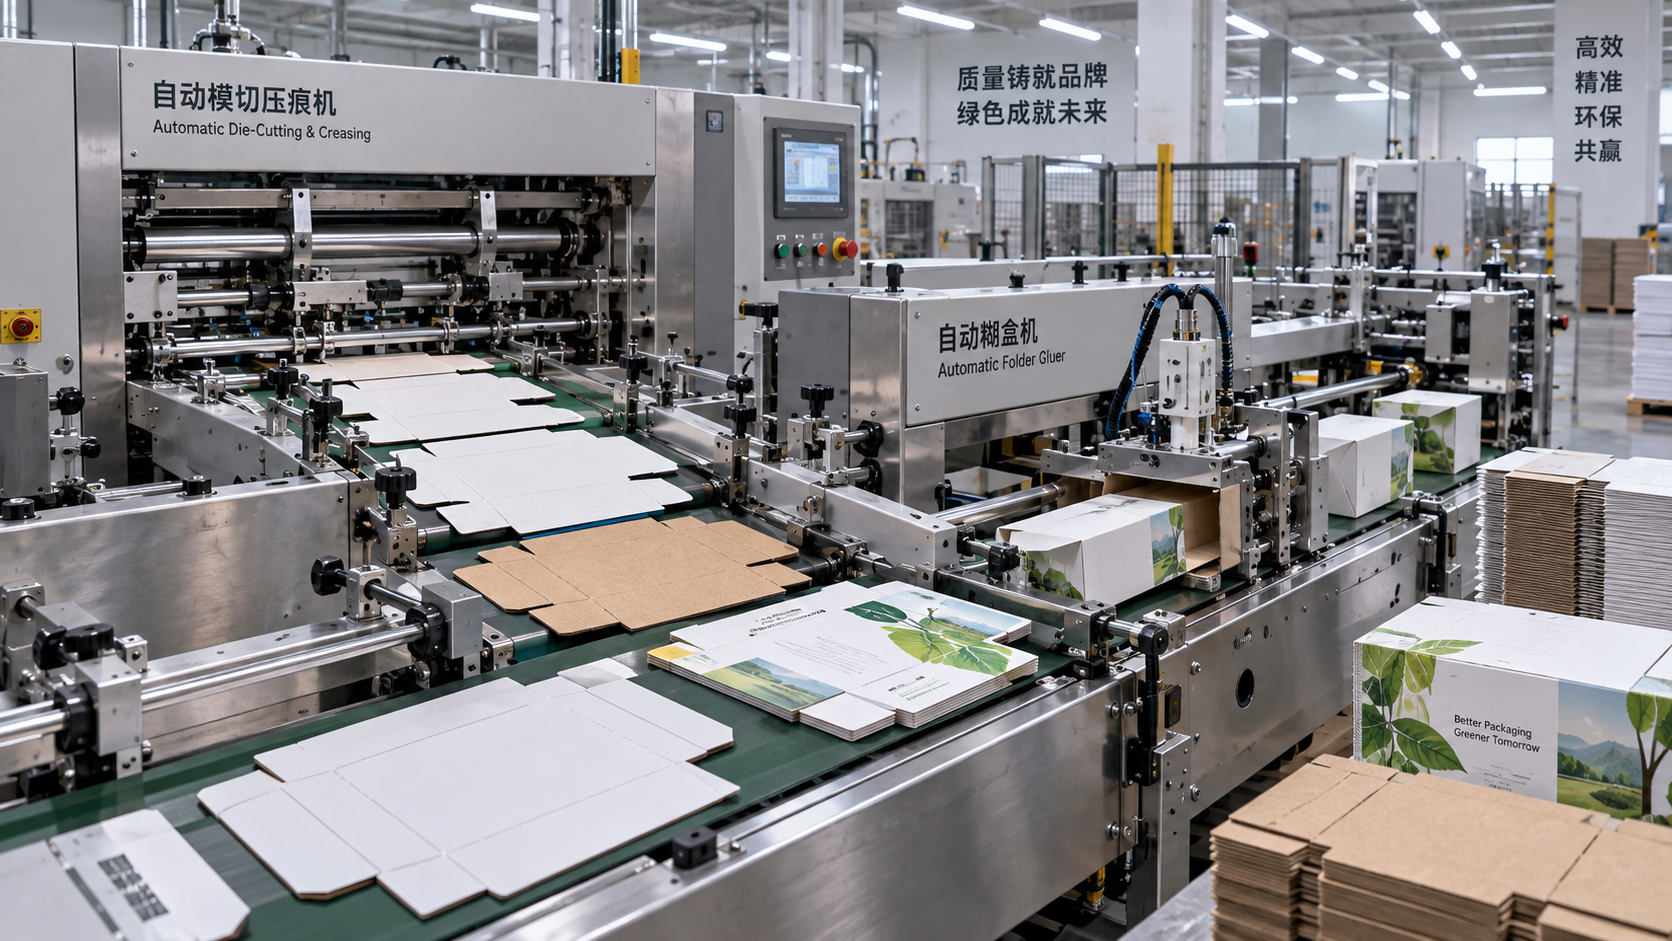
A carton line can be mechanically capable yet commercially unsuitable if its material window is defined too broadly. Paperboard grade affects far more than whether a blank can pass through a feeder. It determines how reliably the blank separates, how much force is needed to crease and cut it, whether folds close on score lines, how adhesive wets the surface, and how much process variation the line can absorb before rejects rise.
For technical evaluators, the practical question is not “Which machine handles paperboard?” Nearly all carton converting machinery can be configured for some range of board. The useful question is: which paperboard grades, constructions, and condition ranges must this line process at the required quality and speed? A folding carton line designed around lightweight coated stock makes different demands from a line converting stiff recycled board, solid bleached sulfate, uncoated kraft, or microflute corrugated material. Selecting on nominal caliper alone is a common source of expensive mismatch.
Start with the material envelope, not the machine brochure
Machine specifications often state a board thickness range and a maximum sheet size. Both figures matter, but they are only the outer boundary of capability. A technical assessment should translate the expected paperboard mix into a working material envelope that includes caliper, basis weight, stiffness, grain direction, surface finish, moisture sensitivity, print coverage, coating, and structural design.
Two boards with the same caliper may behave very differently in a feeder, die-cutter, or folder-gluer. A dense virgin-fiber cartonboard can have high bending resistance and crisp score behavior. A bulkier recycled grade at the same thickness may compress more at the crease, show wider variation in thickness, and require different stripping, folding, or gluing settings. A coated board may feed cleanly but present adhesive challenges on heavily varnished areas. A microflute blank may be dimensionally large and lightweight, but its flute direction and crush sensitivity can dominate the converting process.
That distinction is why a machine rated for a broad “paperboard range” should not automatically be assumed suitable for every grade within it. The upper end of a nominal range is often achieved under controlled conditions, with a relatively simple blank geometry, appropriate tooling, and a speed lower than the headline production rate. The specified range should be treated as the beginning of technical due diligence, not the final selection criterion.
- Define the normal production mix, rather than only the heaviest or lightest grade.
- Identify the grades that generate the highest margin, strictest appearance standard, or greatest annual volume.
- Separate occasional trial materials from materials that must run predictably every shift.
- Record permitted variation in caliper and moisture, especially when sourcing from multiple mills or regions.
- Include printed, coated, laminated, or varnished conditions, since a raw sheet and a finished printed blank do not always convert alike.
Feeding stability is usually the first material-machine constraint
Feeding is often treated as a routine function until material variation exposes its limits. Lightweight folding carton stock may be prone to static, curl, double-sheeting, or inconsistent separation. Stiffer board can resist pickup and may require stronger feeder settings, different suction arrangements, or more controlled pile handling. At the other end of the range, thick board or corrugated blanks can create stack-height, registration, and transfer challenges even where the feeder can physically lift the sheet.
Surface characteristics matter here as much as weight. Smooth coated surfaces, high-coverage ink, aqueous coatings, and varnishes can alter friction between blanks. A feeder setup that performs consistently on uncoated stock may show doubles or missed feeds after a finish changes. Recycled grades can also introduce greater surface and thickness variability, which makes separation settings less forgiving.
For this reason, feeder evaluation should consider the intended board in its real production condition. It is insufficient to confirm that a machine runs an unprinted sample of equivalent thickness. The assessment should include the final print and coating build-up, the intended blank size, and the likely storage condition before conversion. Board curl created during printing, coating, or environmental exposure can affect registering and folding more than a simple grade description suggests.
A useful procurement question is whether the feeder’s adjustment range, sheet-separation system, antistatic provisions, pile lift, and register controls are appropriate for the full operating mix. Another is how repeatable those adjustments are when jobs change frequently. A machine that can be tuned by a specialist for one difficult board may still be a poor fit for a short-run environment with frequent grade changes.
Die-cutting and creasing depend on stiffness, compression, and fiber structure
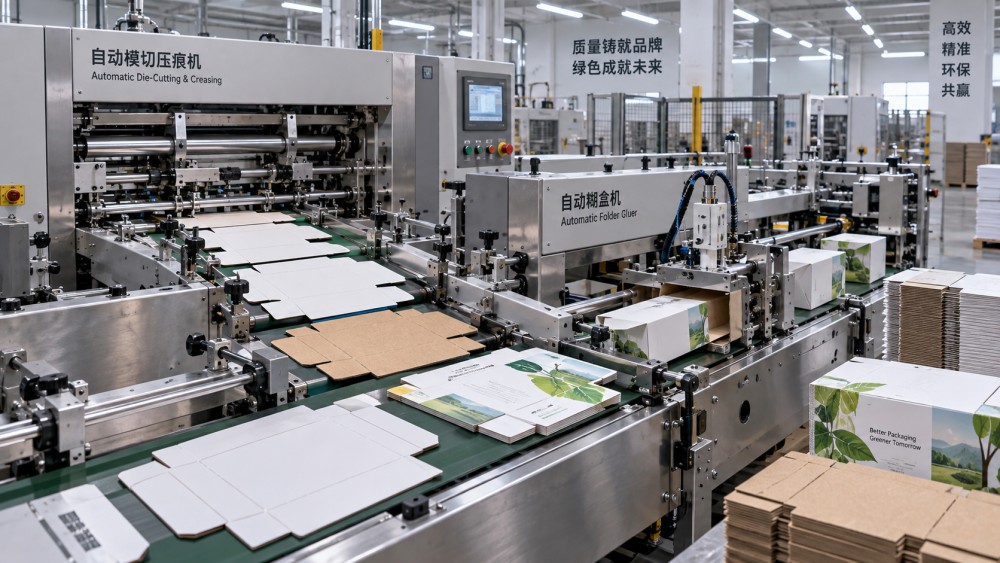
Paperboard grade has a direct effect on the cutting and creasing section. Cutting force rises with material density, caliper, board construction, and blank perimeter. Creasing performance depends on how the board compresses beneath the rule and how the fibers respond along and across the grain. The goal is not simply to create a visible score. The score must guide folding without cracking the printed surface, delaminating the board, weakening the panel, or producing an uncontrolled fold angle.
Lightweight cartonboard can be efficient to cut but may be vulnerable to over-creasing, distortion, and stripping damage. Stiff, high-caliper board may need deeper or more carefully balanced creasing, and it can increase wear on tooling and machine components. Recycled grades may exhibit more variable compression behavior, so settings that create an acceptable score on one batch can produce cracking or weak folding on another. Coated or highly printed surfaces introduce a further risk: a crease that is structurally adequate may still fail an appearance requirement through coating fracture.
Microflute and other corrugated formats require a different evaluation mindset. The material’s thickness alone does not define its convertibility. Flute profile, liner construction, flute orientation relative to the blank, and allowable flute crush all matter. The die-cutting system must achieve clean cuts and reliable creases without reducing the board’s protective performance or creating uneven panels that complicate downstream folding and gluing.
Technical evaluators should therefore review the complete tooling and pressure-control approach. Questions worth resolving include whether the machine offers stable pressure distribution across the sheet, how quickly make-ready adjustments can be made, whether the stripping configuration suits small or intricate waste areas, and how the supplier defines performance at the upper end of the board range. Tooling suppliers should be involved early where the carton contains tight radii, narrow panels, deep embossing, windows, or complex stripping patterns.
Crease quality should be assessed after folding
Inspection directly after die-cutting can be misleading. A score can look clean while still producing cracking, spring-back, skewed panels, or poor squareness once the blank reaches the folder-gluer. The test standard should examine the finished carton: fold alignment, edge appearance, panel geometry, glue seam integrity, and the carton’s ability to erect as intended. This is especially important for cartons carrying premium graphics, heavy ink coverage, or coatings that make surface fracture highly visible.
Folder-gluer selection follows board recovery and carton geometry
Folder-gluer performance is strongly affected by the board’s tendency to recover after bending. Stiff grades can spring open after the fold section unless crease quality, pre-breaking, carrier pressure, and compression length are properly matched. Softer or lower-stiffness board may fold readily but can be more susceptible to scuffing, panel distortion, and loss of dimensional control at high speed.
The folding architecture should be matched to the carton style and board behavior. Straight-line cartons in a stable lightweight grade may run efficiently on a relatively straightforward configuration. Crash-lock bottoms, multi-point cartons, heavy board, coated stock, or irregular structural designs impose a higher demand on pre-folding, transport stability, timing, and compression. A line that appears fast on a simple straight-line sample may offer limited usable speed on a complex carton built from stiff stock.
Grain direction deserves explicit treatment in this stage. Folding parallel to the grain generally behaves differently from folding across it, and carton layouts may include both orientations. The effect becomes more visible as caliper, stiffness, coating weight, and graphic sensitivity increase. Procurement teams should ensure that trials use the actual imposed grain direction of the production layout, rather than a sample blank arranged for the convenience of a demonstration.
Glue selection also belongs in the machinery decision. Board surface energy, coating, varnish, dust level, and absorption affect wetting and bond development. Uncoated absorbent stock can require a different adhesive application balance from dense coated cartonboard. A heavy or highly recovered board may need adequate compression time and pressure before the carton can be packed. If a specification assumes hot-melt, cold glue, or a combination of adhesive systems, the gluer configuration should support the required pattern, temperature control, inspection, and accessible cleaning regime.
Do not confuse maximum speed with usable throughput
The most consequential paperboard decision is often hidden inside a speed assumption. Published machine speed is normally a mechanical capability, while usable throughput reflects feeding stability, registration, make-ready time, die-cutting pressure, blank complexity, folding behavior, glue setting, inspection requirements, and reject handling. A board grade that pushes several sections toward their operating limits can reduce net output substantially even when no individual station is technically overloaded.
This gap is largest when the operation expects a mixed product portfolio. A machine optimized for thin, uniform cartonboard may generate impressive output on long runs but lose efficiency when asked to alternate among lightweight stock, stiff premium board, and coated recycled grades. Conversely, a more robust configuration can be justified when the business requires frequent changeovers, wider material tolerance, or a larger share of difficult structural cartons.
Rather than ask for one speed figure, define performance by production family. For each representative carton, document the board grade, thickness range, blank size, print finish, carton style, tooling requirement, target quality criteria, anticipated run length, and acceptable waste level. Then request a line-speed expectation against that defined job. This makes comparisons between converting platforms more credible and prevents a maximum-speed figure from becoming an implicit production commitment.
A trial should stress the assumptions that the purchase depends on
A meaningful acceptance trial is not a demonstration using the supplier’s preferred stock. It should be designed around the material and carton combinations that will determine the investment outcome. Where the operation buys from more than one paper mill, the trial should include realistic grade variation where possible. Where appearance is critical, samples should carry the intended ink, coating, and varnish system. Where downstream packing is sensitive, converted cartons should be erected and checked in the relevant packing process.
The most revealing test articles are often not the easiest high-volume SKU. They are the cartons at the edge of the operating window: a stiff grade with cross-grain folds, a heavily printed blank susceptible to cracking, a coated surface with demanding glue adhesion, a small carton requiring precise registration, or a microflute format with narrow tolerances. These jobs expose whether a carton converting machinery paperboard specification is genuinely robust or only theoretically broad.
- Measure feed consistency, including doubles, misses, skew, and register drift.
- Inspect cut edges, nicks, waste removal, and tooling-related marking.
- Evaluate crease depth and fold appearance on the completed carton, not only on flat blanks.
- Check glue placement, bond strength, open-carton rate, and compression performance.
- Record setup time, adjustments required, waste during stabilization, and the speed at which quality remains acceptable.
The purchase decision should then be framed around the narrowest critical interaction between material and process. If the business depends on a demanding board grade, the machine must be selected for repeatable operation on that grade, not for its best result on the easiest substrate. When the material envelope is defined clearly and tested through feeding, converting, folding, and gluing as one system, machinery selection becomes a capacity and quality decision grounded in the cartons the operation actually needs to deliver.
Industry Briefing
Get the top 5 industry headlines delivered to your inbox every morning.
Recommended News