How to assess an industrial printing manufacturer's capacity
A press may look impressive at full speed on a showroom floor. The harder question is what happens when it handles your substrates, your artwork, your finishing requirements and an unexpected rush order—all in the same week.
For procurement teams, assessing an industrial printing manufacturer means looking beyond a quoted machine speed or an attractive price. You need evidence of usable output, consistent quality, available capacity and support after installation or delivery. This industrial print buyer guide offers a practical manufacturer assessment framework for comparing suppliers on the conditions that matter to your operation.
One distinction shapes the entire evaluation: are you buying printing equipment, or commissioning a manufacturer to produce printed goods? An equipment supplier must demonstrate that its machine can perform in your plant. A print service provider must show that its existing operation has enough capacity to deliver your orders. Much of the evidence overlaps, but the questions—and contractual safeguards—are different.
Start with the job, not the press brochure
Before requesting quotations, define a representative production profile. A supplier cannot give a meaningful capacity assessment from an annual volume alone. Two buyers ordering the same number of sheets may create very different workloads if one runs a single design and the other changes artwork several times a day.
Your brief should include:
- Expected volumes by week and month, including seasonal peaks and likely order sizes.
- Substrates, thickness ranges, sheet or web dimensions, and any important surface characteristics.
- Artwork complexity, variable-data requirements, color expectations and acceptable tolerances.
- Required finishing, such as die-cutting, creasing, stamping, folding or gluing.
- Delivery locations, turnaround expectations and any traceability or material documentation requirements.
Separate mandatory requirements from preferences. A supplier that can produce excellent samples but cannot handle your peak order window may still be unsuitable. Likewise, a fast press is of limited value if it cannot maintain acceptable print quality on your actual corrugated board.
Turn headline speed into usable capacity
Manufacturers often quote maximum mechanical speed under favorable conditions. That figure is useful for understanding the machine’s potential, but it is not a production commitment. Ask for the assumptions behind it: substrate, coverage, print mode, resolution, job length, finishing arrangement and whether loading and unloading are included.
A more useful planning estimate starts with available production time and subtracts scheduled maintenance, changeovers, cleaning, calibration and other expected stoppages. Apply the expected running speed for your job, then account for startup waste and rejected output. The result is an estimate of saleable output, not simply printed material.
For example, a press may run quickly on long, repeat jobs but spend a much larger share of the day preparing short runs. Digital printing can reduce plate-related setup, yet file preparation, color checks, substrate changes and downstream handling still consume time. Ask the supplier to model your actual mix rather than extrapolating from its best-performing job.
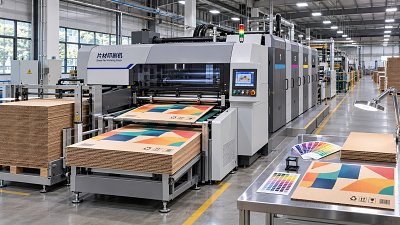
When comparing print service providers, request historical utilization or production records where commercially appropriate, along with a proposed allocation for your work. Existing equipment does not automatically equal available capacity. Check whether the supplier relies on overtime, subcontractors or a single bottleneck machine to meet peak demand.
For equipment purchases, distinguish installed speed from the output your own facility can sustain. Staffing, utilities, material handling and working hours all affect the result. A supplier’s demonstration is a starting point; your operating conditions determine the business case.
Follow the order through the entire workflow
Capacity is constrained by the slowest critical step, not necessarily by printing. A press capable of meeting the order date may still feed work into an overloaded die-cutter or folder-gluer. Ask each candidate to map the route from approved artwork to packed shipment, identifying where work queues, changes hands or leaves the site.
Pay particular attention to these interfaces:
- Prepress: How are files checked, versions controlled, barcodes verified and proofs approved? Who resolves artwork errors?
- Material supply: Can the required paper or board be sourced consistently, and what happens if its properties change?
- Print-to-finish matching: Are registration, drying or curing, cutting and creasing compatible with the intended substrate and final design?
- Post-press capacity: Can die-cutting, stamping and folder-gluing keep pace with the expected job mix, including changeovers?
- Dispatch: Are inspection, packing and transport arrangements included in the stated lead time?
For corrugated packaging, look closely at sheet handling and surface variation. Board flatness, flute profile and print-surface characteristics can affect feeding, image consistency and finishing. A realistic trial should use the board grade and construction specified for the final application, not a convenient substitute without disclosure.
Ask for proof of repeatability, not just a perfect sample
A carefully prepared sample shows what is possible. It does not, by itself, show what can be repeated across shifts, batches and substrate deliveries. Agree on measurable acceptance criteria before a trial, and make sure they reflect the way the finished product will be used.
Depending on the application, criteria may cover color consistency, registration, legibility of small text and codes, print adhesion, rub resistance, cut and crease position, and the integrity of glued areas. For packaging, inspect finished boxes as well as printed sheets: a good print can be undermined by cracking at a fold or inconsistent conversion.
Request a documented quality-control plan that explains where checks occur, how frequently samples are taken, which instruments or methods are used and what happens when a result falls outside tolerance. Ask how the supplier handles traceability, quarantines suspect material and investigates recurring defects.
For an equipment purchase, agree on a factory acceptance test and, where appropriate, a site acceptance test. Specify the test files, substrate, run length, operating conditions and calculation method for accepted output. Record what is excluded, who provides consumables and how any failed criterion will be resolved. A short demonstration run should not be mistaken for evidence of sustained production.
Examine lead times and resilience under pressure
A quoted lead time is only useful when its starting point and dependencies are clear. For printed orders, establish whether the clock begins at purchase order, artwork approval, material availability or receipt of payment. For machinery, separate manufacturing, shipment, installation, commissioning, operator training and final acceptance.
Then test the uncomfortable scenarios. What happens if a printhead, drive component or finishing machine fails? Is there a qualified alternative production route? How quickly can critical spare parts reach your site? If subcontracting is proposed, will you know which work is outsourced and whether the same quality requirements apply?
Ask for a named escalation path and realistic response arrangements rather than relying on a general promise of support. For equipment, check remote diagnostics, local service coverage, technician availability, software support and expected consumable supply. Response time and repair time are not the same thing; both deserve clarification.
Compare costs across the operating life
The lowest quotation can become expensive if it assumes an unrealistic yield or excludes work that your production cannot avoid. Build a common cost model for all shortlisted suppliers, using the same job mix and assumptions.
For equipment, consider purchase price alongside installation, training, ink and other consumables, maintenance, spare parts, software, utilities, waste and operator requirements. For outsourced printing, include tooling or setup charges, proofs, finishing, packaging, freight, storage and the treatment of overruns or rejected goods.
Ask suppliers to identify variable costs and exclusions. If one proposal depends on a higher running speed or lower waste rate, request evidence from a comparable trial. Sensitivity testing is useful: recalculate the economics with lower utilization, more frequent artwork changes or a higher reject rate. A proposal that works only under ideal assumptions carries more risk.
Use a weighted scorecard—but keep evidence visible
A scorecard helps procurement teams compare unlike proposals, especially when technical, operations and finance colleagues value different things. Agree on weights before reviewing final bids. The example below is a starting point, not a universal formula.
Use pass-or-fail gates for non-negotiable requirements, such as a critical delivery window or a required substrate. Otherwise, a low price can conceal a failure that no weighted average should excuse. Record the evidence behind every score and flag claims that remain unverified.
Responsible sourcing deserves the same discipline. If forest certification or regulatory documentation matters to your market, identify the applicable requirement and ask for current, relevant evidence covering the materials and supply chain involved. Do not assume that a broad sustainability statement establishes compliance with every customer or jurisdictional obligation.
Questions to settle before awarding the contract
By the final discussion, the best supplier should be able to explain not only what it can do, but also the conditions under which it can do it. Before signing, confirm:
- What accepted output, quality criteria and delivery dates are being committed to?
- Which substrates, artwork versions and operating assumptions underpin those commitments?
- Who approves proofs, supplies materials and bears the cost of changes or rejected work?
- What capacity or support is reserved for peak demand and equipment disruptions?
- How will performance be reviewed, and what remedies or corrective steps apply if requirements are missed?
A strong assessment leaves room for honest limits. A manufacturer that clearly identifies a bottleneck and proposes a credible plan may be a safer partner than one that agrees to every requirement without supporting evidence. Use the trial, workflow review and contract discussion together to choose the supplier whose demonstrated capacity fits the work you actually need done.
Industry Briefing
Get the top 5 industry headlines delivered to your inbox every morning.
Got questions about the latest insights discussed here, or seeking customized strategic advice for your business? Drop us a line below, and let the think-tank experts at IPPS help you out.
“We respect your privacy. Your information is strictly confidential.”
Recommended News