Can an e-commerce packaging systems manufacturer prove line speeds?
Can an e-commerce packaging systems manufacturer prove line speeds?
An e-commerce packaging systems manufacturer can quote impressive line speeds, but can it demonstrate sustained throughput under your operating conditions? Proof means more than a peak-speed video: it requires timed trials using representative order mixes, board grades, and pack sizes, with rejects, stoppages, and changeovers included in the results.
The short answer is yes—but only when the test measures the system you intend to operate, rather than the machine the supplier finds easiest to demonstrate. A line running identical cartons from a carefully prepared stack proves something useful. It does not establish what happens when an oversized order follows three small ones, a shipping label fails verification, or corrugated stock needs replenishing.
The buying decision should therefore rest on a documented operating envelope: which orders the line can process, at what sustained output, with how many people, and under which material and integration conditions.
Start by defining what “speed” actually measures
A conveyor speed, a box-forming cycle rate, and completed parcels per hour are different quantities. Even “packages per minute” can conceal whether the count comes from the former, the closer, or the final discharge conveyor. Ask where the measurement occurs before comparing quotations.
For procurement, the most useful primary measure is usually accepted, completed parcels divided by the agreed elapsed test time. “Accepted” needs a written definition: correct dimensions, secure closure, readable and correctly associated labels, and any other requirements relevant to the shipment. A closed carton with the wrong shipping label is not good output.
Set the system boundary as carefully as the formula. If the purchase covers dimensioning, box production, packing, sealing, labeling, and discharge, counting output immediately after box production leaves most of the delivery risk unmeasured.
Keep maximum demonstrated cycle rate as a separate diagnostic figure. It helps explain mechanical capability, but it should not replace sustained throughput in the business case.
Give the supplier a workload, not just a target number
A credible trial starts with order data. Provide the distribution of pack dimensions, item counts, product characteristics, and packaging formats—not merely average carton size. Averages hide awkward combinations. Two order populations can share the same average dimensions while creating very different demands on cutting, folding, conveying, and closing.
Include routine work and difficult but legitimate orders. Depending on the application, these may involve shallow boxes, tall narrow packs, multi-item orders, or products that require controlled orientation. Identify unsupported products separately; an agreed exception route is better than pretending every order belongs on the automated line.
Sequence matters too. Grouping identical orders may reduce adjustments and make a demonstration look smooth. If warehouse release logic produces a mixed stream, test that stream. Where batching is proposed, evaluate its effect on order-release timing and work-in-progress rather than treating it as a free productivity gain.
Material specifications deserve equal attention. Record flute profile, board thickness, liner characteristics, permitted moisture condition, and any relevant recycled-content or surface requirements. Lightweight corrugated material may behave differently through feeding, creasing, and adhesive application. Do not accept a trial on premium stock as proof for a lower-cost production specification without further testing.
Build the factory acceptance test around elapsed time
The factory acceptance test, or FAT, should have an agreed protocol before the equipment is presented. Otherwise, the parties may leave the same demonstration with incompatible conclusions about what passed.
Separate engineering setup from the measured run. Allow agreed preparation, recipe adjustment, and warm-up, then identify the exact start and finish conditions. Routine operator intervention during the run must remain visible. If a technician repeatedly adjusts guides or clears minor faults, that is part of the operating result—not background activity.
- Test duration: long enough to expose relevant replenishment, thermal, adhesive, and recovery behavior, with duration justified against the intended duty.
- Staffing: named roles and headcount, including any supplier personnel assisting production.
- Consumables: production-representative board, adhesive, labels, and other materials, with substitutions recorded.
- Interruptions: explicit treatment of jams, starvation, blocked discharge, consumable replacement, and order-data faults.
- Quality checks: defined inspection methods, sampling frequency, and treatment of defects discovered after discharge.
There is no universal test duration that proves every installation. A short run may validate basic functions but never reach a board replenishment or label-roll replacement. If a continuous trial cannot cover those events, add witnessed tests and report their time impact separately.
For illustration only, suppose a line produces 2,700 accepted parcels during a 60-minute window containing six minutes of stoppages. Its sustained result is 45 parcels per minute. Dividing by the 54 running minutes produces 50 parcels per minute, which answers a different question. Both figures can be useful; only clearly labeled denominators prevent confusion.
Find the bottleneck beyond the box-making module
An integrated packaging line can have several competing constraints. Product induction may struggle with irregular arrivals. A dimensioner may request rescans. The box-making module may keep pace while the closer waits for adequate bonding conditions. Downstream, a label applicator or parcel sorter can restrict the entire system.
This is where a process map becomes more useful than another speed claim. Show every transfer point, queue, reject path, and control handshake from order release to accepted discharge.
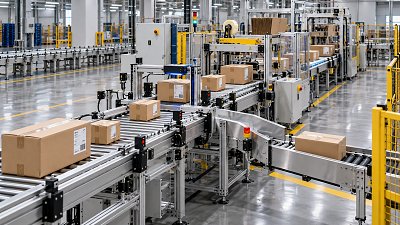
Buffers can absorb short disturbances; they cannot correct a persistent capacity mismatch. Watch queue levels throughout the trial. A test that begins with empty downstream conveyors and ends with accumulated parcels may demonstrate temporary storage rather than sustainable output.
Include controlled interruption and restart scenarios. What happens when the downstream conveyor stops? Does the system preserve the relationship between order, carton, and shipping label? Can it recover without manual reconciliation? Lost tracking after a stop can be more damaging than the stop itself.
IPPS’s coverage of digital printing, corrugated board production, and post-press equipment points to a useful evaluation principle: paper conversion and information handling must be assessed together. Accurate cutting and reliable folding do not compensate for a failed order-data interface.
Ask for evidence that can be reconciled
A summary dashboard is convenient, but it should be backed by exportable records. Request timestamped machine states, counter readings, alarm histories, reject events, recipe changes, and relevant order identifiers. Where multiple controllers are involved, verify that their timestamps can be aligned.
The records should explain the physical result: how many orders entered, how many accepted parcels left, how many were rejected, and what remained inside the system. Reintroduced parcels must not inflate accepted output. Rejects that require manual recovery also create work that belongs in the operating assessment.
Continuous video can help resolve disputed events, especially around feeding, replenishment, and discharge. It supplements logs rather than replacing them. A close-up of the fastest module rarely reveals whether another operator is continuously rescuing the process outside the frame.
Treat overall equipment effectiveness, or OEE, cautiously when comparing proposals. Suppliers may use different ideal cycle times or classify losses differently. Ask for the underlying availability, performance, and quality calculations. A single percentage without those definitions is not a dependable selection criterion.
Keep factory proof separate from site acceptance
A successful FAT reduces uncertainty; it does not prove the installed warehouse system. Site conditions introduce actual upstream feeding, production network behavior, warehouse software interfaces, utilities, operators, and downstream equipment.
The site acceptance test, or SAT, should confirm performance within that environment. Preserve the same output definitions wherever possible so factory and site results remain comparable. Record any differences in workload, materials, staffing, or system boundaries rather than quietly changing the benchmark.
Responsibility for integration losses needs particular care. If the manufacturer excludes delays caused by warehouse software, define how those delays will be identified and logged. Equally, the supplier should not be held responsible for an upstream process operating outside agreed conditions. Clear interfaces protect both parties.
Turn the agreed proof into contract language: workload definition, accepted-output threshold, quality limits, permitted staffing, test conditions, and retest procedure. Specify how failures are corrected and what evidence closes them. Any commercial remedies should be reviewed against the actual agreement and applicable law.
Choose the repeatable result, not the most impressive moment
A manufacturer that qualifies its speed claim is not necessarily offering a weaker system. Explaining which pack sizes constrain output, which materials need validation, and which orders require bypass handling is more useful than promising one rate for everything.
When comparing bids, prioritize demonstrated output across your workload, recovery behavior, labor demand, and the completeness of the evidence. A higher peak rate may justify additional investment where demand and downstream capacity support it. In another facility, easier replenishment and fewer interventions may produce the better operating result.
Before committing to an e-commerce packaging systems manufacturer, ask for the proposed acceptance protocol alongside the quotation. If the supplier can explain what will be counted, what will remain on the clock, and how the result will be verified, there is a credible basis for evaluation. If those questions remain unanswered, the advertised speed is still a claim—not proven capacity.
Industry Briefing
Get the top 5 industry headlines delivered to your inbox every morning.
Got questions about the latest insights discussed here, or seeking customized strategic advice for your business? Drop us a line below, and let the think-tank experts at IPPS help you out.
“We respect your privacy. Your information is strictly confidential.”
Recommended News