Which post press solutions protect rigid boxes from scuffing?
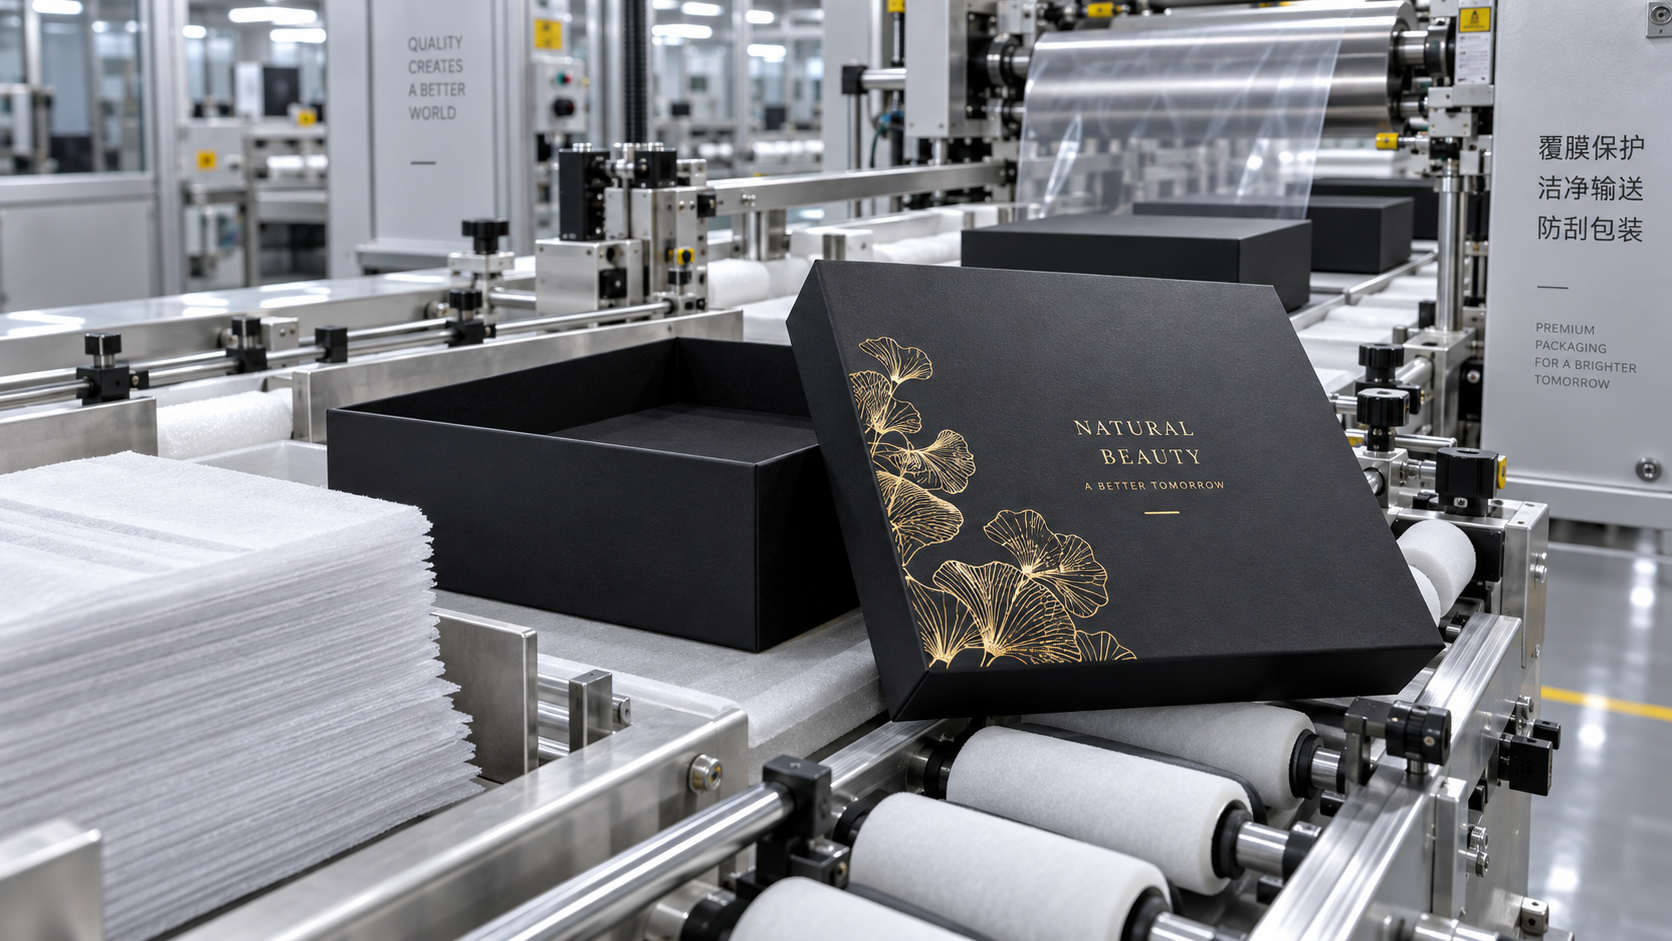
A premium rigid box can leave the finishing line looking flawless and still arrive at packing with rubbed corners, dull panels, or visible drag marks around the lid edge. The risk rises when dark solids, matte surfaces, metallic decoration, soft-touch films, or tightly fitted telescopic components are involved. In these jobs, scuffing is rarely solved by one “stronger coating.” It is controlled by matching the surface finish, board construction, converting sequence, drying or curing conditions, and material handling method.
The most reliable post press solutions rigid boxes depend on are usually a layered system: a suitably abrasion-resistant laminate or coating, protected decorative effects, clean die-cut and stripping conditions, well-controlled glue application, and low-friction movement through assembly and packing. The correct choice depends on where the damage occurs. Surface abrasion during blank handling requires a different response from edge whitening at creasing, foil scratching during stacking, or rub marks created after the box has already been erected.
Start by identifying the scuff pattern
Before specifying a film, varnish, or machine modification, inspect several damaged boxes under the same light used for product approval. A scuff can look like a coating failure while actually being caused by an exposed board edge, excessive pile pressure, contamination on a belt, or a lid that fits too tightly over the base.
This distinction prevents a costly but ineffective response. For example, adding a tougher overprint varnish will not correct marks made by rough metal guides after the coating has cured. Likewise, replacing a protective film may not solve visible corner wear when the lid compresses against an oversized base during repeated opening and closing.
Choose the protective layer according to finish and contact load
Protection starts at the printed wrap or printed board surface. The practical question is not simply whether to use lamination or coating, but which finish can tolerate the actual contact it will receive in converting, rigid box assembly, packing, retail handling, and distribution.
Film lamination for high-contact premium surfaces
Lamination is often the most dependable route where rigid boxes have large exposed panels and repeated friction is expected. A matte, gloss, or soft-touch film creates a physical barrier between ink and external contact. It can also stabilize printed solids that would otherwise show abrasion quickly. However, films behave differently under rubbing. A very tactile matte or soft-touch surface may provide the desired luxury feel while remaining sensitive to fingermarks, pressure polishing, or scratches from hard edges. It should not be assumed that “soft-touch” automatically means “scuff-proof.”
When evaluating a laminated structure, confirm the film’s abrasion behavior, bond quality, fold performance, and compatibility with later foil stamping, embossing, gluing, and wrapping. The adhesive layer matters as much as the film: poor bonding can create edge lifting, bubbles, or delamination at turn-ins, especially around sharp rigid-box corners. Test converted samples rather than only flat sheets, because corner wrapping places the surface under stress that a flat rub test may not reproduce.
Aqueous and UV coatings where film is not preferred
Water-based or UV-curable coatings can provide useful scuff resistance while preserving paper feel, reducing added film, or maintaining a preferred visual effect. They are especially relevant for designs where full lamination would weaken texture, alter color appearance, interfere with downstream decoration, or conflict with a defined material strategy.
Coating selection must account for the ink system and the intended finishing sequence. A coating that looks hard and dry may still mark under concentrated pressure or may crack along a deep score. UV systems can offer strong surface resistance, but their cure level, flexibility, and adhesion must suit the board and fold geometry. Water-based coatings may be preferable for certain paper-based constructions, yet they require sufficient drying before sheets are stacked or sent to later processes. Premature handling can cause blocking, offset, and gloss changes that resemble scuffing.
Use a coating as a protection layer, not as a substitute for poor material handling. On dark, uncoated-looking designs, an invisible coating may reduce rub but will not eliminate scratches generated by debris on conveyor belts or excessive stack pressure.
Protect decorative effects before they enter high-friction stages
Foil stamping, embossing, debossing, spot coatings, and metallic inks make rigid boxes more vulnerable because they create surfaces with different hardness, height, and friction. A raised decorative area can receive concentrated force when blanks are stacked. Metallic layers may reveal scratches more readily than surrounding print, even where the physical damage is slight.
Sequence planning is therefore part of scuff prevention. Where a decorative operation must remain exposed, avoid sending finished sheets through unnecessary transfer stages. Use clean separators or controlled pile formation where practical, and review whether the decoration sits in a likely contact zone: lid corners, side panels that slide against forming tools, or areas facing adjacent boxes in a shipper.
In some designs, a protective clear layer over printed decoration is appropriate. In others, that layer may reduce foil brilliance, change the tactile effect, or complicate later bonding. The evaluation should include actual production-order samples with the complete finish stack, not isolated foil or coating tests. A visually acceptable flat sample can still fail once it is wrapped around board and subjected to edge turn-in pressure.
Creasing and die-cutting can create damage that looks like abrasion
Rigid boxes often use printed wrap sheets that are cut, creased, and folded around greyboard or chipboard. When a score is too aggressive, poorly aligned, or incompatible with the board and coating build, the outer surface can fracture at the fold. On dark colors this may appear as a pale line. It is often incorrectly blamed on post-assembly rubbing.
Check the relationship between board caliper, grain direction, crease rule and channel geometry, coating flexibility, and fold direction. A crease should guide the wrap cleanly without crushing the decorative face or forcing a brittle coating to stretch beyond its tolerance. Die-cutting pressure also needs attention. Excessive pressure can bruise the sheet, weaken the surface at the score, or create rough edges that later abrade adjacent components.
- Confirm that the score is centered and consistent across the sheet.
- Inspect fold lines immediately after creasing, before wrapping or gluing begins.
- Separate cracking from actual surface transfer by checking whether the mark follows the score exactly.
- Review knife, rule, and channel wear when defects worsen gradually through a run.
- Keep stripping waste and paper dust away from finished printed faces.
Precision die-cutting is valuable here not merely for shape accuracy, but because stable scoring and clean stripping reduce the number of downstream contacts required to correct, rework, or manually handle damaged pieces.
Rigid-box forming needs controlled contact, not just faster output
During wrapping and box assembly, the printed surface meets guides, belts, folding fingers, pressure rollers, corner tools, and operators’ handling points. These contacts are necessary, but their condition determines whether an abrasion-resistant finish remains intact. Dirt, dried adhesive, worn rollers, exposed fastener edges, or overly hard contact pads can create repeatable marks in exactly the same location on every box.
A useful diagnostic method is to track the first stage at which a mark appears. Retain samples after cutting, after decoration, after wrapping, after base or lid forming, and after final packing. Once the first affected sample is found, inspect every surface that touches that panel. This is more efficient than adjusting several materials at once.
Particular attention should go to pressure at turn-ins and corner folds. Excessive force can burnish a matte surface, damage foil, or push adhesive toward visible areas. Too little force can produce loose wrap edges that later catch and scuff. The target is uniform contact with tools that are clean, correctly aligned, and appropriate for the finished surface. Where a box style has a tight corner radius or thick board, the wrap material and adhesive open time must allow forming without repeated repositioning.
Glue control affects appearance as well as bond strength
Adhesive contamination is a frequent hidden contributor to scuff complaints. Stray glue on guides, belts, pressure tools, or packing surfaces can create drag marks, gloss variation, and surface tearing. Excess adhesive can squeeze from turn-ins, while insufficient adhesive encourages lifted edges that are vulnerable during later handling.
Set glue volume for the actual absorbency of the wrap and board, then verify the result at corners and overlaps. The relevant question is whether the adhesive forms a stable bond without migrating into visible areas or transferring to another box. Drying time also matters: a box moved too soon may be structurally formed but still vulnerable to surface marking under stack pressure.
Do not ignore fit between lid, base, insert, and shipper
A rigid box can pass the finishing line unmarked and become scuffed during its first functional use. Telescopic lids, shoulder boxes, drawer sleeves, and fitted inserts create repeated contact at edges and panels. A tight fit may be perceived as premium at first, yet it can rub the printed wrap every time the lid is removed or replaced. Small dimensional variation in board thickness, wrap buildup, adhesive thickness, or humidity can make that fit inconsistent.
Assess assembled boxes by opening and closing them repeatedly under normal handling, then inspect the contact areas. Look for polished bands, corner rubbing, ink transfer, or friction noise. Check whether an insert pushes outward against the lid or whether a product protection component shifts and drags across the inner surface. These are construction issues, not finish-only issues.
Packaging after assembly deserves the same scrutiny. Boxes should not move freely against one another in transit, but excessive compression can also damage soft or matte surfaces. Dividers, tissue, protective sleeves, and packing orientation may be justified for high-value finishes. Their material should itself be clean and non-abrasive; rough recycled board, poorly cut inserts, or dusty protective sheets can defeat the purpose.
A practical evaluation route before release
For a new box design, compare candidate systems on converted samples rather than making a decision from a swatch book. Build samples with the intended print coverage, protective layer, decorative effects, board, glue, crease pattern, and assembly method. Then expose them to the contacts that the box will actually experience: pile handling, guide transfer, wrapping pressure, lid movement, nesting, and packed-box friction.
- Define the visual failure limit first: visible whitening, loss of matte appearance, scratched foil, ink transfer, or edge wear may have different acceptance thresholds.
- Map the process sequence and mark every surface contact after printing.
- Choose the least complex protective finish that withstands those contacts without damaging the required appearance or fold behavior.
- Run a short production-condition trial and retain samples at each stage.
- Inspect not only the face panel but also corners, scores, overlaps, and areas hidden until the box is opened.
- Document machine settings, drying or curing conditions, material batch details, and handling changes that affect the result.
The strongest selection is usually not the hardest coating or the thickest film. It is the finish and process combination that remains stable through the actual post-press path. For rigid boxes with dark matte wraps, exposed foil, sharp corners, or close-fitting components, surface protection should be specified together with die-cutting, wrapping, glue control, and packing conditions. Treating these as separate decisions is where preventable scuffing usually begins.
Industry Briefing
Get the top 5 industry headlines delivered to your inbox every morning.
Recommended News