What Should Packaging Automation Acceptance Testing Include?
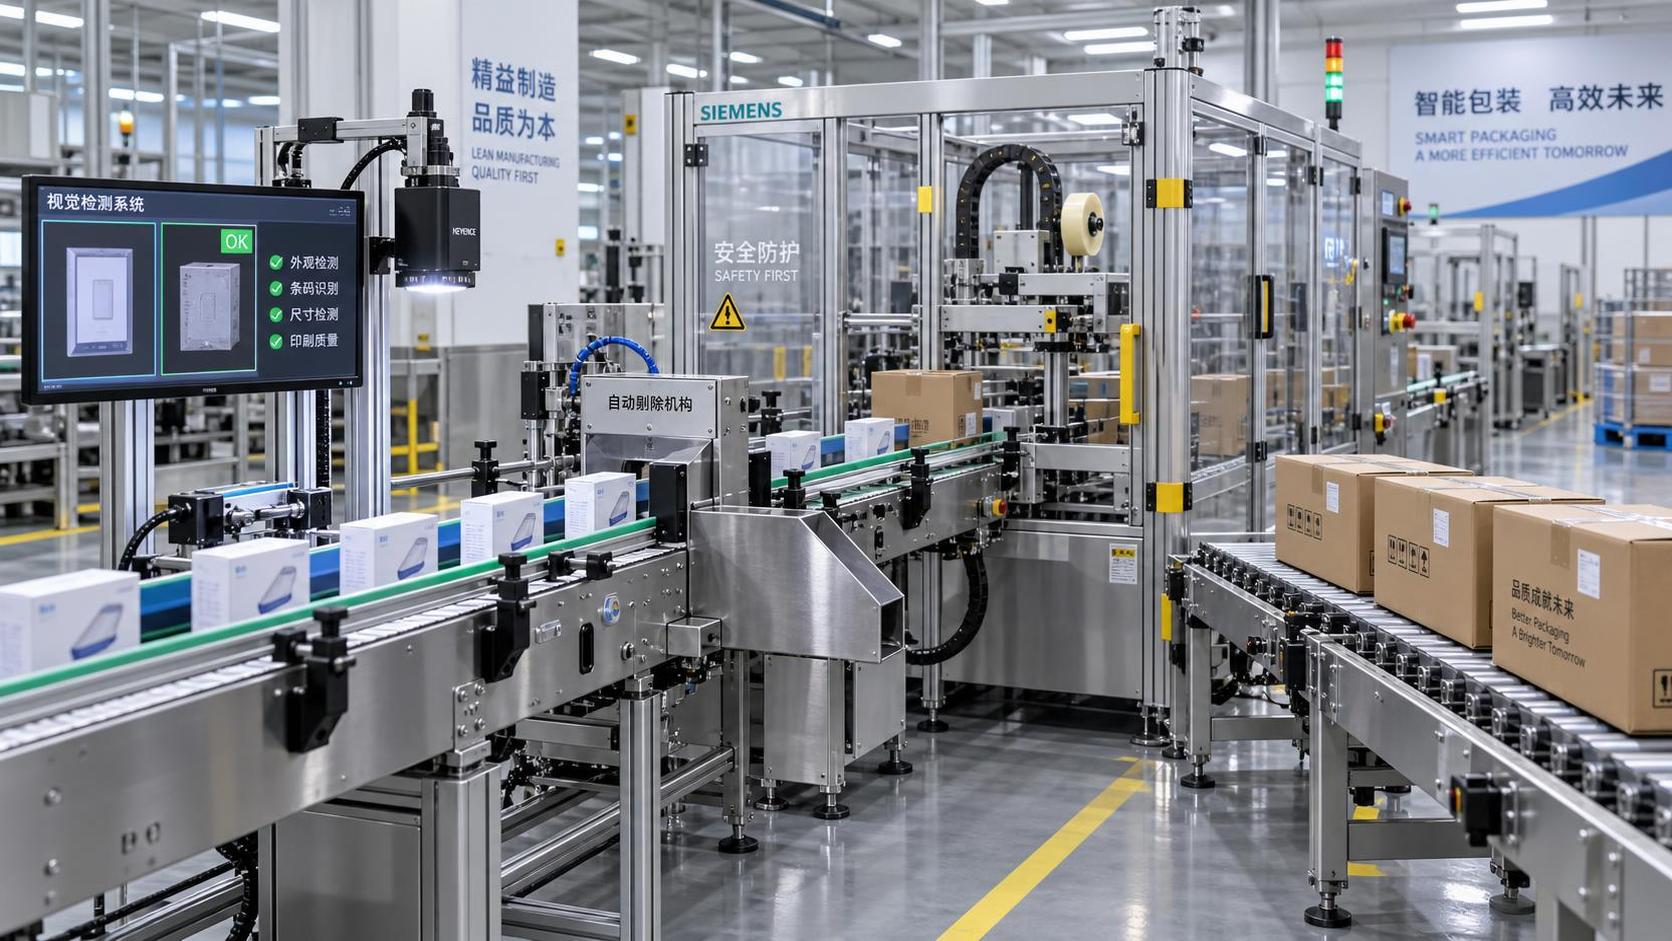
Packaging automation acceptance testing should prove more than that a machine can run products at a stated speed. It should demonstrate that the installed system can repeatedly produce saleable packs, safely and traceably, using the real materials, product mix, utilities, operators, and upstream/downstream interfaces that will exist in production.
The decisive distinction is between a demonstration and an acceptance test. A demonstration may show a case packer, cartoner, folder gluer, robotic palletizer, or automated tissue packaging line operating under favourable conditions. Acceptance testing establishes whether the agreed performance is sustainable within defined operating limits. If the test conditions are vague, a supplier and buyer can both claim success while holding very different assumptions about what the equipment has actually been proven to do.
A credible acceptance plan therefore needs measurable criteria, controlled test conditions, documented exceptions, and clear rules for retesting. It should cover mechanical performance, pack quality, safety, controls, integration, maintainability, and the practical realities of changeovers and recovery from normal production disturbances.
Start with an acceptance specification, not a speed target
The acceptance protocol should be agreed before final machine build or, at the latest, before factory acceptance testing. It needs to convert commercial promises into testable definitions. “High efficiency,” “easy changeover,” “works with recycled board,” and “operator friendly” are not acceptance criteria until they are tied to a product, a method, a measurement, and an allowable result.
The specification should identify the exact equipment boundary. In a packaging cell, that boundary may include infeed conveyors, orienting devices, printers and vision systems, product handling robots, cartoning or case-packing equipment, adhesive systems, reject stations, pallet conveyors, safety guarding, electrical panels, supervisory controls, and interfaces to plant systems. Ambiguity at handoff points is a frequent source of dispute: a cartoner can meet its own cycle rate while starving because the upstream feeder cannot provide a stable pitch, or a palletizer can be blamed for a problem caused by unstable cases from the sealer.
Each test requirement should state:
- the product, pack format, substrate, adhesive, ink, label, or consumable to be used;
- the operating speed or throughput basis;
- the required duration of the run;
- the quality characteristics to be checked and how they are measured;
- the permitted number and category of faults, rejects, and interventions;
- the responsible party for data capture and sign-off;
- the corrective-action and retest process if a criterion is not met.
Throughput needs particular care. Packs per minute, cases per minute, sheets per hour, and pallets per hour can all be valid metrics, but only if the count point is defined. The most useful measure is generally good output at the agreed discharge point, excluding units rejected for equipment-induced defects. A gross machine cycle count can conceal reject volume, manual rework, or short stops that materially reduce usable production.
Factory acceptance testing should de-risk the build
Factory acceptance testing (FAT) is not a substitute for site acceptance testing, because the production environment is not yet replicated. Its purpose is to verify that the machine has been built to specification and that fundamental functions work before shipment. Catching mechanical, electrical, software, guarding, and access issues at this stage is usually less disruptive than correcting them after installation.
FAT should inspect the build against approved drawings and the bill of scope: frame construction, guarding, electrical enclosures, cable identification, pneumatic routing, lubrication points, sensors, actuators, installed format parts, and access for cleaning and maintenance. For systems handling printed cartons or corrugated blanks, inspection should include critical guides, squaring mechanisms, vacuum transfer points, folding rails, creasing contact surfaces, and glue-application components. Small alignment errors at these points can become quality losses at production speed.
Controls testing should confirm the operation of every normal and abnormal sequence. This includes start-up, controlled stop, emergency stop, reset logic, jam detection, low-material alarms, product absence detection, reject confirmation, machine-emptying routines, and restart behaviour. The test should not merely confirm that an alarm appears on the HMI. It should confirm that the system enters the correct safe state, gives a meaningful fault message, prevents unsafe restart, and recovers without creating an untracked product or packaging defect.
Where machine safety functions are part of the supply, the validation records should align with the applicable legal and technical framework for the destination market. ISO 12100 is commonly used as a basis for machinery risk assessment and risk reduction; ISO 13849-1 may be relevant to safety-related control systems; IEC 60204-1 addresses electrical equipment of machines. Their applicability depends on the equipment, jurisdiction, contractual scope, and conformity route. A certificate or component label alone does not demonstrate that the installed safety function has been correctly implemented and validated.
FAT should also verify documentation quality. Electrical schematics, pneumatic diagrams, software backups, parts lists, operating manuals, maintenance instructions, safety information, and format-part drawings must match the delivered configuration. A line can be mechanically sound yet costly to support if drawings are incomplete, software versions are uncontrolled, or spare-part identities are unclear.
Site acceptance must use production-real conditions
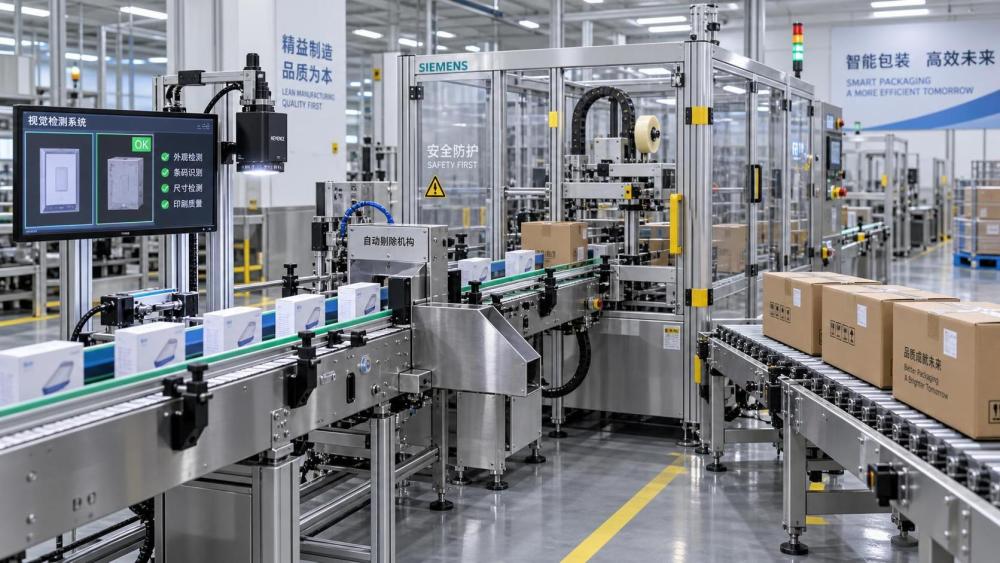
Site acceptance testing (SAT) is where packaging automation proves its operational value. The installation should be complete, utilities stable, interfaces commissioned, and safety systems active before a meaningful run begins. Testing an isolated machine with hand-fed product, temporary compressed-air arrangements, or bypassed downstream equipment can be useful for debugging, but it should not be treated as final acceptance.
Real packaging materials matter. Carton stiffness, corrugated board caliper, flute profile, liner quality, coating, print varnish, moisture content, glue open time, label release force, film coefficient of friction, and product geometry all influence machine behaviour. A system proven on ideal samples may perform differently on the full material tolerance expected from qualified suppliers.
The test set should represent the approved operating range, not just the easiest stock-keeping unit. This does not mean every SKU must receive a long performance run. It means the acceptance matrix should include the formats that stress different mechanisms: the smallest and largest pack, the lightest and heaviest product, the most flexible carton blank, the most demanding label position, the highest stack pattern, or the format with the tightest tolerance. A supplier cannot reasonably be expected to guarantee unapproved or materially changed packaging materials, so the material specifications themselves should be controlled.
Utilities are equally important. Compressed air pressure and air quality, electrical supply stability, vacuum capacity, network availability, adhesive temperature, cooling water where applicable, and dust extraction can all affect performance. Acceptance records should note actual utility conditions during the run. Otherwise, a later performance failure may be difficult to attribute fairly.
Measure performance as a production system
A long run at nominal speed remains central, but it should not be the only performance test. The run needs to reflect the line’s intended operating pattern, including normal replenishment, permissible operator actions, and functioning quality checks. The protocol should define whether planned activities such as magazine loading, glue refill, label roll replacement, or pallet discharge are included in the result. Excluding all routine activities can create a rate that is technically correct but operationally misleading.
Useful measures include good units produced, reject rate by defect category, unplanned stop count, cumulative downtime, mean recovery time for defined faults, and manual intervention frequency. Overall equipment effectiveness is sometimes used, but it should be applied carefully during acceptance. Its availability, performance, and quality assumptions must be agreed; otherwise it becomes a composite number that obscures the underlying cause of loss.
Short stops deserve separate attention. A packaging line can appear to meet average output over a limited trial while accumulating sensor faults, unstable product transfers, misfeeds, or intermittent glue alarms. These events may be recoverable, yet they consume labour and reduce real capacity. The acceptance log should classify them by cause: equipment design, tuning, material variation within specification, utility interruption, upstream supply, downstream blockage, operator action, or external event. This classification is not about assigning blame prematurely. It is essential for deciding whether a result proves the machine or merely reflects a favourable test window.
Pack quality must be inspected beyond visual appearance
Acceptance testing should define what constitutes a good pack at every relevant level: product presentation, primary pack integrity where in scope, carton or case geometry, closure quality, coding, labeling, and pallet stability. Inspection should be performed at normal speed and after deliberate stops and restarts, because defects often occur during transitions rather than during steady running.
For folding cartons and corrugated cases, checks may include squareness, flap position, glue pattern and bond integrity, compression or deformation, correct tuck engagement, correct blank orientation, print or label position, barcode readability, and absence of scuffing or fibre tear-out. For automated tissue packs, sealing consistency, pack dimensions, film tracking, tear features, count accuracy, and product compression effects may be relevant. For palletized loads, acceptance may need to verify layer registration, pack orientation, pallet overhang, stretch-wrap application, top-sheet handling, and the integrity of the load through the intended transfer route.
Sampling should be sufficiently structured to detect trends. Inspecting only a handful of finished packs at the end of a run can miss progressive drift caused by glue temperature, vacuum contamination, guide wear-in, printhead performance, or tension changes. When a critical quality characteristic is measured, the instrument, method, sampling point, and acceptance tolerance should be documented. If packaging carries regulated product information, code verification and reconciliation rules need to be included rather than left to a later operational procedure.
Changeovers and recoverability reveal whether automation is usable
A machine that reaches its target rate on one format but requires excessive adjustment to change products may not deliver the flexibility assumed in the investment case. Changeover acceptance should test the agreed formats with the specified format parts, recipe selection, adjustment points, and staffing level. The clock should start and stop at clearly defined conditions, such as the last accepted pack of the previous format and the first sustained sequence of accepted packs of the next format.
The result should include more than elapsed time. It should show whether settings are repeatable, whether the selected recipe produces usable initial packs without extensive trial-and-error, whether tools are required, and whether components can be installed incorrectly. An electronically stored recipe does not guarantee a repeatable changeover if mechanical guides, glue nozzles, vacuum cups, or sensor positions still require undocumented manual tuning.
Recovery testing is similarly revealing. Planned scenarios may include an empty carton magazine, product accumulation, a missing label, a glue alarm, a blocked discharge, a rejected pack, or a safety-gate opening. The objective is not to force abusive conditions. It is to verify safe machine response, containment of affected product, alarm clarity, restart steps, and return to stable output. A robust system should not turn a minor disturbance into a lengthy manual clearing exercise or allow questionable packs to pass unnoticed.
Integration and data integrity need explicit tests
Packaging automation increasingly depends on data exchange with printers, vision systems, warehouse controls, production reporting platforms, and enterprise systems. Acceptance should verify the actual messages and failure states, not only the existence of a network connection.
Relevant checks may include recipe download and version control, product-code selection, print-data transfer, barcode or OCR verification response, reject tracking, production counts, downtime codes, batch or lot association, user-access levels, audit trails where required, and behaviour after a network interruption. If a line must prevent mixed products or incorrect artwork, the test should demonstrate the interlock under an intentionally incorrect instruction—not simply show that correct data produces a correct pack.
Physical interfaces also require verification at full operating speed. Conveyor accumulation logic, line balancing, speed reference signals, transfer heights, spacing, and handshakes with upstream and downstream systems can determine whether a cell performs as designed. A single machine’s acceptance result should not be used to infer line performance unless the contracted scope includes the integrated line.
Safety, maintainability, and handover are acceptance items
Safety validation must include more than an inspection of guards. Test emergency stops, interlocked doors, light curtains, safety scanners, two-hand controls where fitted, safe torque-off functions, restart prevention, and stored-energy isolation procedures. Verify that access needed for clearing jams, replenishing materials, cleaning glue systems, changing format parts, and servicing print or inspection devices can be performed without creating foreseeable exposure to moving machinery, sharp tooling, hot surfaces, adhesives, or unexpected motion.
Maintainability affects uptime from the first production week. Acceptance should check access to wear components, sensor adjustment, lubrication, cleaning points, filter replacement, and common fault areas. It should confirm that critical spares are identified and that preventive-maintenance intervals are tied to real machine components rather than generic statements. Training should be evidenced by demonstrated capability: operators should safely run, stop, change, and recover the equipment; maintenance personnel should be able to isolate energy, interpret diagnostics, restore approved settings, and manage software backups.
Final acceptance should not erase open issues. A punch list is appropriate for minor items that do not compromise safety, contracted performance, product quality, documentation, or legal conformity. Each item needs an owner, due date, and closure criterion. Material defects should remain outside final acceptance until corrected and retested under the relevant condition.
Well-designed packaging automation acceptance testing protects both sides of a supply contract. It gives the equipment provider a defined target and controlled conditions for proving the system. It gives the operating business evidence that capacity, quality, safety, integration, and recovery behaviour are fit for real production. The strongest result is not a machine that briefly reaches a headline speed; it is a documented system that produces conforming packs reliably across the conditions it was purchased to handle.
Industry Briefing
Get the top 5 industry headlines delivered to your inbox every morning.
Recommended News