When coated paper improves the perceived quality of paper packaging
When Coated Paper Improves the Perceived Quality of Paper Packaging
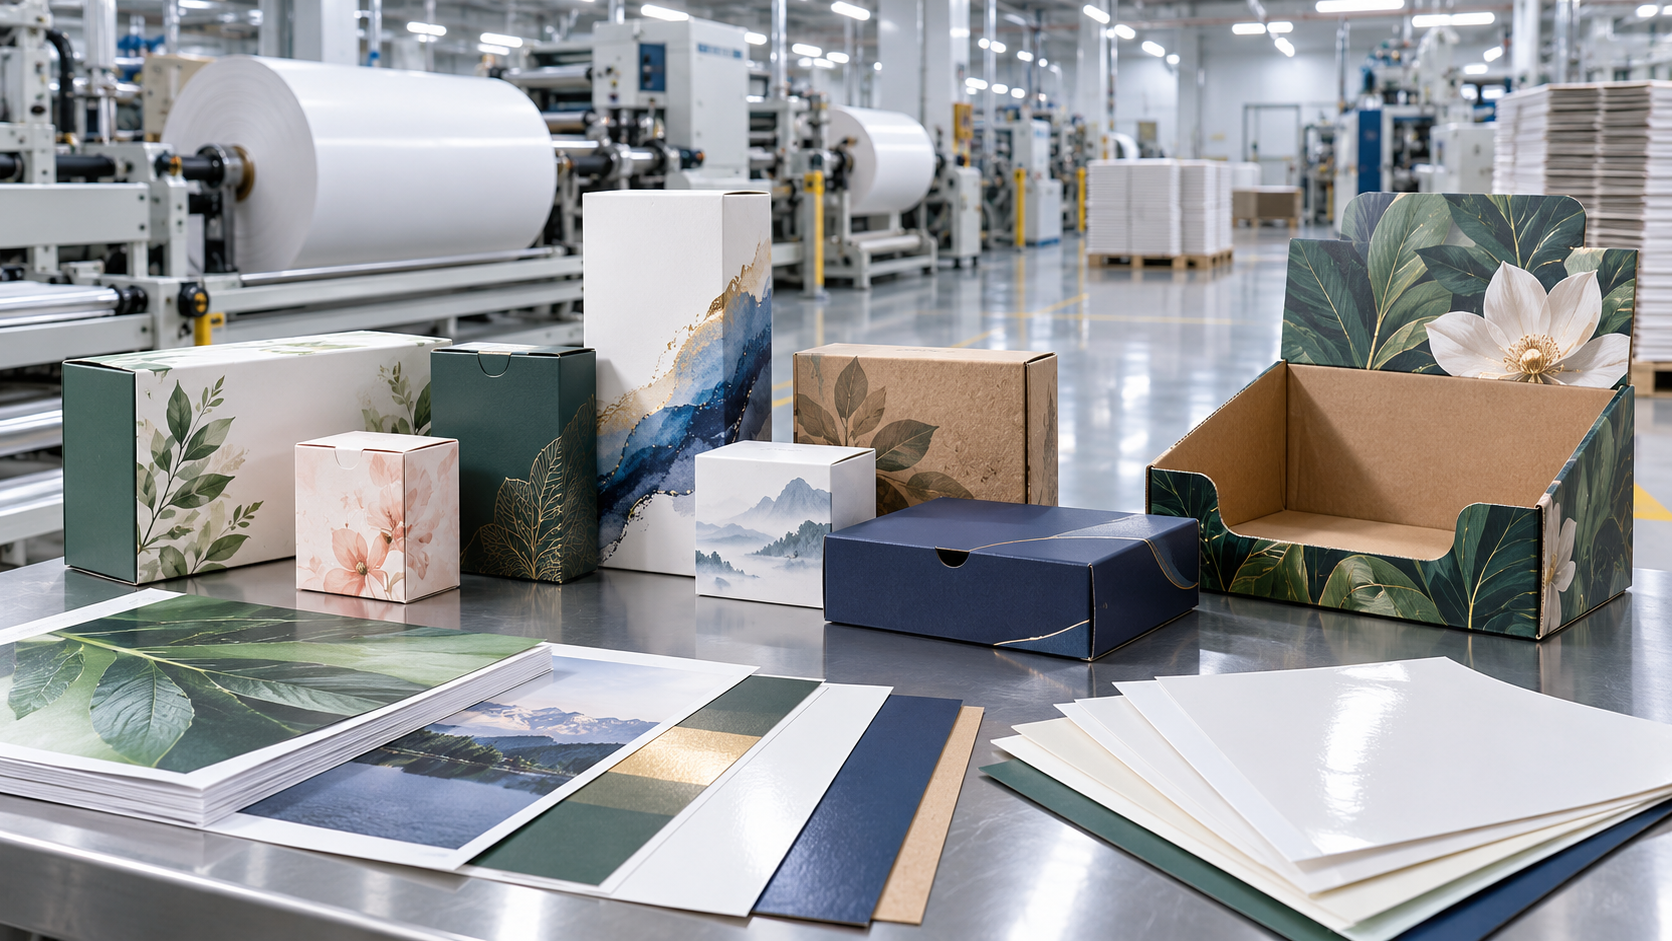
Packaging quality is often judged before a product is touched, opened, or understood. A clean color field, a sharply defined logo, and a controlled sheen can make a folding carton appear deliberate and valuable. For business evaluators reviewing paper packaging investments, coated paper is therefore not simply a print substrate choice. It is a decision about how reliably a brand can communicate quality across retail shelves, e-commerce deliveries, short-run campaigns, and different production sites.
The appeal is easy to understand. A coated surface limits uncontrolled ink absorption, helping graphics retain edge definition, color density, and visual consistency. But coating is not a universal upgrade. On the wrong carton structure, with an unsuitable finishing sequence, or in a supply chain where scuff resistance matters more than gloss, it can add cost without improving the customer’s experience. The better question is not “Should this package use coated paper?” It is “At which moment does the surface quality influence buying confidence enough to justify the material and process choices behind it?”
Perceived quality begins with how the printed surface behaves
Coated paper and paperboard have a pigment-and-binder layer that creates a more even printing surface than many uncoated grades. In practical packaging work, this means ink tends to remain closer to the surface rather than sinking deeply into the fiber network. Fine typography is more legible, photographic images appear more controlled, and solid brand colors are less likely to look patchy because of local variation in absorbency.
That difference matters most when a design depends on visual precision. Cosmetics, personal care, premium food, consumer electronics accessories, seasonal gift packs, and branded pharmaceutical secondary packaging often use small type, subtle tonal transitions, metallic effects, or densely managed brand color systems. A rougher surface may be entirely functional, but it can make delicate graphics feel less resolved. In a category where the product itself cannot be evaluated until after purchase, that visual uncertainty can work against the brand.
The strongest effect is rarely “more shine equals more premium.” In fact, excessive gloss can make some products look generic, particularly in natural, wellness, craft, and environmentally positioned categories. What buyers often read as quality is control: a smooth matte surface with dense black type, a restrained silk finish, or a gloss accent used only on a logo can look more expensive than a fully glossy carton. Coated paper expands these options because it gives printers and converters a more predictable starting point.
Where the investment is usually easiest to defend
Coated paper performs best when the package is expected to sell, reassure, or differentiate—not merely contain. A branded retail carton is the obvious example, but there are less obvious ones. Direct-to-consumer subscription packs can benefit from a coated outer sleeve or printed insert because the unboxing moment is part of retention and social sharing. Promotional packs with frequent artwork changes may benefit when digital printing is used to avoid plate-making and support localized or personalized graphics. A coated printable face can help short-run digital work look closer to the intended brand standard, provided the ink, primer, and drying conditions are validated together.
Another common application is litho-laminated corrugated packaging. Corrugated board supplies cushioning and compressive structure; the coated top sheet carries the visual burden. This division of labor is important. Asking a shipping-grade corrugated liner to reproduce fine imagery at a premium standard is usually unrealistic. Using a well-chosen coated label or litho sheet can allow a brand to preserve presentation quality while keeping the protective function of the corrugated format.
For high-speed post-press operations, a consistent surface can also reduce avoidable visual variation after printing. Die-cutting, creasing, foil stamping, embossing, and folding-gluing all reveal weaknesses that are not always obvious on a flat press sheet. If the printed face scuffs easily, cracks around a fold, or loses adhesion where glue is applied, the package may look poor despite excellent press output. The value of coated paper is therefore linked to the full converting route, not just to the pressroom proof.
A smooth surface does not automatically create a better package
The most common evaluation mistake is treating coating as a finish rather than a system variable. A coated grade can improve print appearance, but it can also be less forgiving when the packaging will be heavily folded, exposed to abrasion, or processed at speed. Coating weight, board construction, fiber direction, moisture condition, ink coverage, varnish, and scoring geometry can all affect the finished result.
Consider a dark, full-coverage carton with several tight folds. It may look excellent as a press sheet and still show light-colored cracking at the creases after die-cutting and folding. The issue is not always the paper alone. It can arise from an overly aggressive score, unsuitable board caliper, insufficient flexibility in the ink-and-varnish stack, or a mismatch between the coating and the folding condition. A meaningful test is not a flat sample viewed under ideal light. It is a production-representative blank that has been printed, finished, creased, folded, glued, packed, and handled.
The same caution applies to glossy surfaces in logistics-heavy applications. Gloss can elevate shelf presence, yet highly reflective packs show scratches and fingerprints readily. When cartons are packed tightly, conveyed quickly, or shipped through multiple distribution points, a lower-gloss coating or protective overprint varnish may deliver a better real-world result. Evaluators should ask to see samples after rub testing and pack-out simulation where possible, not just immediately after production.
Digital printing makes substrate selection more consequential
Industrial digital printing has made it practical to produce multiple designs, regional versions, and short promotional runs without conventional plate workflows. That flexibility is valuable, but it raises the importance of substrate qualification. Different digital print engines interact with coated paper in different ways. Inkjet systems may require a receptive coating or primer to control dot spread, drying, and adhesion. Dry-toner processes can introduce heat and pressure that influence curl or surface behavior. UV-curable systems demand attention to cure, odor considerations where relevant, and fold durability.
The operational detail that often gets missed is web and sheet stability. At production speed, the appearance of a printed package depends on far more than file resolution. Tension variation, moisture imbalance, coating-side orientation, static, and calibration discipline can influence registration and color consistency. This is particularly relevant for digitally printed top sheets that will be laminated to corrugated board, where any distortion can become more noticeable after bonding.
For evaluators comparing equipment or production routes, the right request is a realistic application trial. Use the intended artwork, representative ink coverage, the planned finishing sequence, and the actual board or paper grade. A generic print test can establish that a machine works. It does not establish that the package will meet commercial expectations.
Sustainability questions need a more careful answer than “coated or uncoated”
Coated paper is sometimes treated as inherently less aligned with fiber-based packaging goals. That is too simplistic. The environmental profile of a finished pack depends on the base fiber, coating chemistry, inks, adhesives, barriers, laminations, recovery infrastructure, and the rules of the market where it is sold. A paper package with a coating may still fit established paper recycling streams in some circumstances, while a visually simple pack may become more difficult to recycle because of added films, heavy barrier layers, or complex construction.
The practical approach is to define the function before judging the material. Does the package need grease resistance, moisture protection, high gloss, tactile softness, or simply better color reproduction? Each requirement should be challenged separately. If premium graphics are the only reason for a plastic laminate, a coated paperboard with an appropriate varnish may offer a simpler route. If the product genuinely requires a high-performance barrier, reducing the structure to a “paper-only” claim may be misleading and may compromise protection.
FSC claims, EUDR-related due diligence expectations, recyclability guidance, and local labeling rules should also be reviewed against current market-specific documentation. These are not details to add late in artwork approval. They can affect sourcing, print claims, and the evidence needed from suppliers. The most credible sustainability decision is one that can be explained through the actual pack structure, rather than through a broad material slogan.
A practical way to evaluate coated paper before committing
A useful assessment starts with the consumer-facing moment. Is the carton viewed from a distance on a shelf, photographed for online retail, handled at a beauty counter, or opened at home after a courier delivery? The answer determines whether color vibrancy, texture, structural stiffness, scratch resistance, or unboxing detail deserves the larger share of the budget.
Then follow the package through the factory. Confirm the print process, drying or curing route, embellishments, die-cutting conditions, folding direction, glue areas, packing method, and expected distribution environment. Coated paper should be assessed after each of these stages. A very attractive press proof has limited value if it causes inconsistent glue bonding or increases rejects at the folder-gluer.
It is also worth separating visible quality from over-specification. A secondary transit carton, hidden inside a shipping case and carrying only handling information, may not need a premium coated face. By contrast, a small product sleeve seen in every product photograph may justify careful substrate and finish selection even if its material area is modest. Applying coating selectively across a packaging portfolio is often more rational than trying to make every paper component look premium.
This systems view is increasingly relevant across digital print, corrugation, and post-press operations. Print quality comes from the interaction of ink behavior, substrate surface, web or sheet control, converting accuracy, and the way the final carton survives handling. Industry intelligence that connects these stages is more useful than a material comparison made in isolation.
The decision is really about credibility
Coated paper improves perceived quality when it makes the package look intentional, reproducible, and appropriate to the product inside. It is especially effective where fine graphics, controlled color, premium finishing, and a polished first impression influence purchase or brand trust. It is less compelling when durability, cost discipline, or a deliberately natural aesthetic matter more than surface refinement.
Before approving a grade, evaluate a converted sample rather than a paper swatch. Fold it, rub it, glue it, pack it, and inspect it under the lighting conditions where customers will actually see it. That small amount of discipline usually reveals whether coated paper is a genuine quality lever—or simply an expensive way to make the specification look more sophisticated.
Industry Briefing
Get the top 5 industry headlines delivered to your inbox every morning.
Recommended News